When do PAO synthetic lubricants suit low-temperature operation?
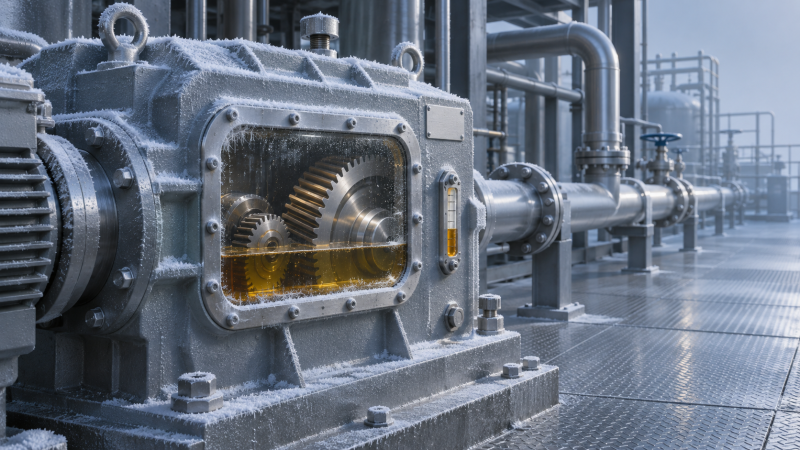
PAO synthetic lubricants are strong candidates for low-temperature operation when the limiting problem is getting oil to flow, pump or reach loaded surfaces during a cold start. Their low-temperature fluidity can make them useful in gearboxes, bearings and hydraulic systems exposed to prolonged cold, particularly where a conventional lubricant becomes too viscous for reliable circulation.
The base oil alone does not establish suitability. A finished PAO-based lubricant must meet the equipment’s viscosity requirements at both startup and operating temperature, deliver the required additive performance, and remain compatible with seals and other materials. The decisive comparison is therefore between complete formulations under the equipment’s actual temperature and operating conditions—not between base-oil names alone.
Start with the coldest operating condition, not the ambient temperature
The relevant temperature is the temperature of the lubricant when the equipment must start or continue operating. That may differ substantially from the outdoor air temperature. A machine in an unheated enclosure can cool over a long shutdown, while a continuously running gearbox may retain heat even when the surrounding air is much colder.
For selection, distinguish at least three conditions: the lowest oil temperature after a realistic shutdown, the temperature at which the machine must start under load, and the normal stabilized operating temperature. Where equipment is moved between environments or experiences intermittent use, the cold-soak duration matters because the oil in the reservoir, lines and housings may not cool at the same rate.
The immediate cold-start question also varies by system. A gearbox may need enough fluidity for oil to reach bearings and gear meshes. A hydraulic unit must draw fluid through the suction line without excessive inlet restriction. A circulating lubrication system must deliver oil through filters and narrow passages at an acceptable rate. In each case, a low pour point is useful information, but it does not by itself demonstrate that the system will function.
Why PAO can help—and what it cannot guarantee
Polyalphaolefin, or PAO, is a synthetic hydrocarbon base oil. Compared with many conventional mineral base oils, suitable PAO grades can retain useful flow characteristics at lower temperatures. PAOs can also provide a favorable viscosity-temperature relationship: viscosity changes with temperature, but a suitable formulation can remain more manageable over a wide operating range.
That creates a potential advantage when an oil must circulate after a cold soak yet still provide adequate viscosity after the machine warms up. It does not mean that every PAO lubricant flows better than every non-PAO alternative. Base-oil viscosity, formulation choices and additives all influence the finished fluid. A carefully formulated non-PAO product may meet a particular cold-start requirement, while a PAO product of the wrong viscosity grade may not.
PAO also does not eliminate the need for heating. If the specified minimum startup temperature is below the lubricant or equipment limits, a reservoir heater, insulated lines, a warm enclosure or a controlled startup procedure may still be necessary. Conversely, if reliable heating already keeps the oil above the critical temperature, changing base-oil chemistry may offer little operational benefit.
Read viscosity data at both ends of the temperature range
An ISO viscosity grade identifies a viscosity range at 40°C; it is not a cold-start performance rating. Two ISO VG 46 lubricants can have different viscosities at low temperature, even though both fall within the same grade at 40°C. A comparison based only on the grade printed on the label can therefore miss the difference that matters during startup.
Request the finished lubricant’s viscosity at temperatures relevant to the application, or a viscosity-temperature chart supported by suitable test data. Compare the result with equipment limits for starting viscosity, pump inlet conditions and operating viscosity, where the manufacturer provides them. Data measured near the intended temperature is more useful than an extrapolation far outside the range of available measurements.
The operating-temperature check is equally important. Choosing a thinner oil solely to improve cold flow can reduce lubricant film thickness once the equipment is hot. In a gearbox, that can affect the separation of loaded gear and bearing surfaces; in a hydraulic system, it can increase internal leakage or compromise lubrication of the pump. The acceptable range depends on the component design, load, speed and manufacturer’s requirements.
Viscosity index can help describe how strongly viscosity changes with temperature, but it is not a complete selection criterion. A higher viscosity index does not establish the actual viscosity at the minimum startup temperature, nor does it establish whether the additive package or mechanical performance is suitable. Compare the measured or credibly calculated viscosities at the temperatures that matter.
Pour point is a screening value, not a working limit
Pour point indicates the lowest temperature at which an oil is observed to flow under a defined test procedure. It does not specify the temperature at which the oil can be pumped through a particular filter, drawn into a pump without problems, or delivered quickly enough to a bearing. An oil can be above its pour point and still be too viscous for the equipment.
Use pour point to eliminate clearly unsuitable candidates, then seek application-relevant viscosity and pumpability evidence. Where the duty is critical, the margin between the lowest expected oil temperature and the product’s demonstrated operating capability should reflect measurement uncertainty, temperature variation and the consequences of inadequate lubrication. There is no universal temperature margin that replaces a system-specific assessment.
Different machines expose different cold-start limits
Gearboxes and bearings
In a splash-lubricated gearbox, cold oil must be moved by the rotating components and reach the surfaces that need it. Excessive viscosity can increase starting torque and reduce effective oil distribution. In a circulating system, the limiting point may instead be the pump, filter or a small supply passage. The same oil can behave differently in these two arrangements.
For bearings, evaluate how oil is supplied as well as its viscosity. A reservoir temperature alone does not prove that oil has reached a remote bearing after startup. Supply-line length, filter condition and the time before the bearing carries substantial load all affect the risk. At operating temperature, the oil must still satisfy the bearing and gearbox requirements for viscosity and additive performance.
A PAO gear oil can be a sensible candidate for equipment that starts cold and later runs hot, but the gear design and load remain decisive. A product intended for lightly loaded bearings should not be substituted for an extreme-pressure gear lubricant simply because both contain PAO. Check the equipment manufacturer’s lubricant specification and any required gear-performance approvals or test results for the finished product.
Hydraulic systems
Hydraulic cold starts are often constrained by the pump’s inlet conditions. Thick fluid increases resistance through the suction line and inlet strainer, potentially preventing the pump from filling properly. Noise, unstable operation and damage can result; changing the oil will not necessarily solve a restriction caused by line sizing, a blocked strainer or an unsuitable startup procedure.
Compare the cold viscosity against the pump manufacturer’s startup and operating limits, taking care not to treat a permitted short-duration startup viscosity as a continuous operating limit. Then confirm that the fluid remains within the required viscosity range when the reservoir is hot. Response of valves, filters and other components should also be considered, particularly where the system must perform precise movements soon after startup.
Hydraulic performance is more than viscosity. Anti-wear properties, air release, foaming behavior and water-handling characteristics must match the system’s requirements. A PAO-based hydraulic fluid with good cold flow is not automatically interchangeable with every other fluid of the same ISO viscosity grade.
Check the finished formulation and material compatibility
PAO base oils are relatively nonpolar. Formulators may combine them with other base stocks and additives to achieve the required additive solubility and seal behavior. The proportions and formulation are product-specific, so conclusions about compatibility should be drawn from the finished lubricant and the materials in the equipment, not from PAO chemistry alone.
Check elastomers, seal compounds, coatings, plastics and any other wetted materials against the lubricant supplier’s compatibility information and the equipment manufacturer’s restrictions. Seal compatibility is not simply a question of whether a material is generally described as compatible: temperature, exposure time, seal condition and the specific compound can affect the result. Where failure would have significant consequences, a representative compatibility test may be justified.
Additives also need scrutiny. A lubricant designed for cold flow must still provide the wear protection, corrosion control and oxidation performance required in service. For shared lubrication systems, confirm that one formulation meets the requirements of all lubricated components. A fluid optimized for a hydraulic pump, for example, should not be assumed suitable for a heavily loaded gearset without supporting evidence.
Assess the changeover, not just the candidate oil
Replacing an existing oil introduces mixing and cleanliness questions. Residual oil can remain in coolers, lines, filters, housings and low points after a drain. If the old and new fluids have different base stocks or additive systems, unintended mixing can affect appearance or performance. A product being described as PAO-based does not establish compatibility with the fluid already in the machine.
Obtain a compatibility assessment for the specific products, including any flushing medium. Decide whether a simple drain and refill, a flush, or a more thorough cleaning procedure is appropriate for the equipment and the contamination risk. The changeover plan should also address filter replacement, disposal of the displaced fluid and how the new fill will be identified to prevent later top-ups with an incompatible product.
Cold operation can also reveal problems that an oil change alone will not fix. Water contamination, restricted filters, excessive suction-line losses and inadequate heaters may compromise startup regardless of base oil. Investigating these conditions before a conversion helps distinguish a fluid limitation from a system limitation.
What evidence supports a defensible selection?
A useful comparison starts with a small set of candidate finished lubricants that meet the equipment specification. For each candidate, request the technical data sheet and, where necessary, supporting information covering:
- Viscosity at the relevant cold-start and stabilized operating temperatures, together with the applicable test methods or calculation basis.
- Pour point and any available low-temperature pumpability or application-specific test data.
- Compliance with the equipment manufacturer’s lubricant requirements, including the necessary wear or gear-performance properties.
- Compatibility guidance for the existing lubricant, seals and other wetted materials.
- Operating limits, handling requirements and any restrictions on mixing or changeover.
Published data should then be checked against the complete system. If the minimum oil temperature, pump limits or actual operating temperature are unknown, resolving those gaps may be more valuable than comparing additional products. Where the consequences of a failed start are substantial, a controlled trial can confirm whether the selected formulation delivers acceptable startup behavior, oil supply and operating temperatures under representative conditions. Monitoring should follow the equipment manufacturer’s limits and an agreed test procedure.
The best case for a PAO formulation is one in which its measured low-temperature behavior closes a demonstrated gap without sacrificing hot-running viscosity, component protection or compatibility. If an existing approved lubricant already meets those conditions with adequate margin—or if the real constraint is a heater, filter or pump inlet—the more appropriate decision may be to correct the system rather than change the base oil.
Facing technical bottlenecks in manufacturing or looking for more efficient industrial solutions? Leave your details below and let the engineering experts at G-PME solve them for you.
We respect your privacy. Your information is strictly confidential.
Recommended News
 When do PAO synthetic lubricants suit low-temperature operation?PAO synthetic lubricants can improve cold-start flow—but are they right for your equipment? Learn how to assess viscosity, compatibility and performance.
 EIA Raises Oil Forecasts, Sees Brent Near $100 for Rest of 2026EIA oil forecasts put Brent near $100 for the rest of 2026. Explore potential impacts on lubricant costs and procurement, and what buyers should verify.
 Americas Base Oil Weekly: High Crude and Feedstock Costs Compound Supply TightnessAmericas base oil supply is tightening as crude and feedstock costs rise. Explore the impact on Group II+ and Group III availability, pricing and purchasing.
 Stonepeak Completes 65% Castrol Acquisition; Former Shell CEO to ChairStonepeak's 65% Castrol acquisition brings new leadership as former Shell CEO Ben van Beurden becomes chair. Explore potential implications for lubricant buyers and suppliers.
 LANXESS and BPCL to Explore Immersion Cooling Fluids and Advanced LubricantsLANXESS and BPCL are exploring immersion cooling fluids and advanced lubricants. Discover what the proposed collaboration could mean for buyers and suppliers.
 How to qualify a catalyst manufacturer for synthetic oil productionQualify a catalysts manufacturer for synthetic oil production with practical checks for performance, batch quality, and scale-up. Learn how to reduce risk and select a reliable supplier.
 China’s Base Oil Imports Hit 2026 Low in September; Top Three Suppliers Account for 82.5%China’s base oil imports hit a 2026 low of 67,400 tonnes in September, with three origins accounting for 82.5%. Explore the data and implications for sourcing and supply risk.
 How to verify batch quality with an industrial lubricating oils exporterBuying from an industrial lubricating oils exporter? Learn how to verify batch test results, sampling, and traceability to reduce purchasing risks and protect equipment.
 Are Synthetic Lubricants Worth the Higher Upfront Cost?Are synthetic lubricants worth the higher upfront cost? Discover when lower maintenance, longer oil life, and energy savings justify the premium—and how to calculate your return.
 Choosing a Synthetic Machine Oil Manufacturer: Specs, Testing, and TraceabilityChoose a synthetic machine oil manufacturer with confidence. Learn how to verify specs, testing, and batch traceability to reduce production risks and secure reliable supply.
 When do industrial lubricants for compressors need oil analysis?Industrial lubricants for compressors need oil analysis at baseline, under harsh operating conditions, and after warning signs. Learn how testing prevents downtime and protects equipment.
 When organic chemicals are suitable feedstocks for synthetic lubricantsOrganic chemicals can unlock high-performance synthetic lubricants. Learn how purity, stability, compatibility, and supply control shape reliable industrial formulations.
 What to check before choosing an industrial lubricating oils factoryIndustrial lubricating oils factory selection guide: compare quality control, formulation fit, traceability, technical support, and total cost to reduce downtime risks.
 Can Synthetic Lubricants Be Mixed with Mineral Oils?Can synthetic lubricants be mixed with mineral oils? Discover compatibility risks, safe top-up practices, and expert guidance for protecting industrial equipment.
 How to assess a lubricants manufacturer's batch traceabilityLubricants manufacturer batch traceability: learn how to audit records, controls, CoAs, packaging, and recall readiness to reduce supply risk and protect uptime.
 When do synthetic gear lubricants justify their higher upfront cost?Synthetic gear lubricants can lower lifecycle costs in high-load, hot, or hard-to-service gearboxes. Learn when premium performance delivers real ROI.
 When should industrial lubricating oils be replaced?Industrial lubricating oils: learn when condition, contamination, heat, and oil analysis signal replacement to protect equipment, reduce downtime, and improve reliability.
 FDA Tightens Filing Rules for Synthetic Food-Contact LubricantsFDA Tightens Filing Rules for Synthetic Food-Contact Lubricants: learn how the 2026 FDA update impacts import compliance, toxicology files, certification gaps, and U.S. market access.
 REACH SVHC Update Targets PAHs in Synthetic OilsREACH SVHC Update Targets PAHs in Synthetic Oils: learn how ECHA’s new PAH listing affects EU exports, SCIP notification, compliance planning, and supply chain risk before February 2027.
 How to Choose Synthetic Gear Lubricants for Load, Temperature, and Service LifeSynthetic gear lubricants selection guide: learn how to match load, temperature, and service life to the right formula for better gearbox protection, longer drains, and smarter maintenance decisions.
 Synthetic Lubricants for CNC Machines: How to Choose for Speed, Heat, and Tool LifeSynthetic lubricants for CNC machines improve spindle speed stability, heat control, and tool life. Learn how to choose the right fluid for precision, uptime, and lower wear.


Search News
Popular Tags