Can Synthetic Lubricants Be Mixed with Mineral Oils?
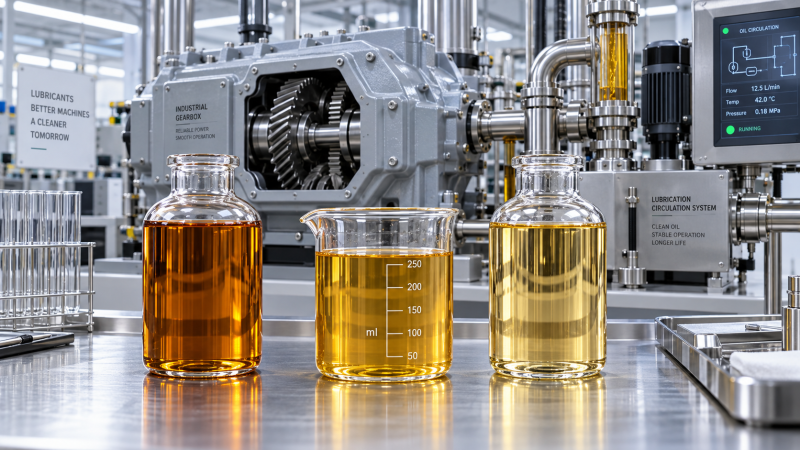
Sometimes—but only when the specific formulations are confirmed compatible. “Synthetic” and “mineral” describe broad base-oil families, not a reliable compatibility verdict. A synthetic lubricant based on polyalphaolefin (PAO), for example, may blend reasonably well with many mineral oils. A polyalkylene glycol (PAG) lubricant may separate from mineral oil or create serious operational problems. Even where the base oils are mutually soluble, additive interactions, viscosity changes, seal response, and the equipment manufacturer’s requirements can make mixing unacceptable.
For industrial equipment, the practical rule is simple: do not treat an oil top-up, an accidental cross-contamination event, and an intentional formulation change as the same decision. A small, documented amount of compatible oil may be manageable. An uncontrolled mixture in a critical gearbox, hydraulic system, compressor, turbine, bearing circulation system, or vacuum pump can shorten lubricant life and obscure the condition of the asset.
Why the label “synthetic” is not enough
Mineral oils are refined from petroleum and commonly use Group I, Group II, or Group III base stocks. Synthetic lubricants may be formulated from PAO, PAG, esters, silicones, phosphate esters, alkylated naphthalenes, or other specialized fluids. These fluids differ substantially in polarity, solvency, water behavior, viscosity-temperature response, oxidation resistance, and compatibility with elastomers and additive packages.
That is why the question “Can synthetic lubricants be mixed with mineral oils?” cannot be answered by comparing the words printed on two product labels. The relevant question is whether the exact lubricant in service is compatible with the proposed replacement or top-up oil under the actual operating conditions.
A useful distinction is often missed: miscibility is not the same as functional compatibility.
- Miscibility means two fluids form a stable, visually uniform mixture rather than separating into layers.
- Compatibility means the mixture can still meet the equipment’s requirements for viscosity, film formation, oxidation resistance, corrosion protection, demulsibility, air release, foam control, filterability, and seal performance.
Two oils can appear clear and homogeneous in a container yet still perform poorly after exposure to heat, pressure, moisture, entrained air, metal surfaces, and long drain intervals.
Which synthetic base oils are most likely to mix with mineral oil?
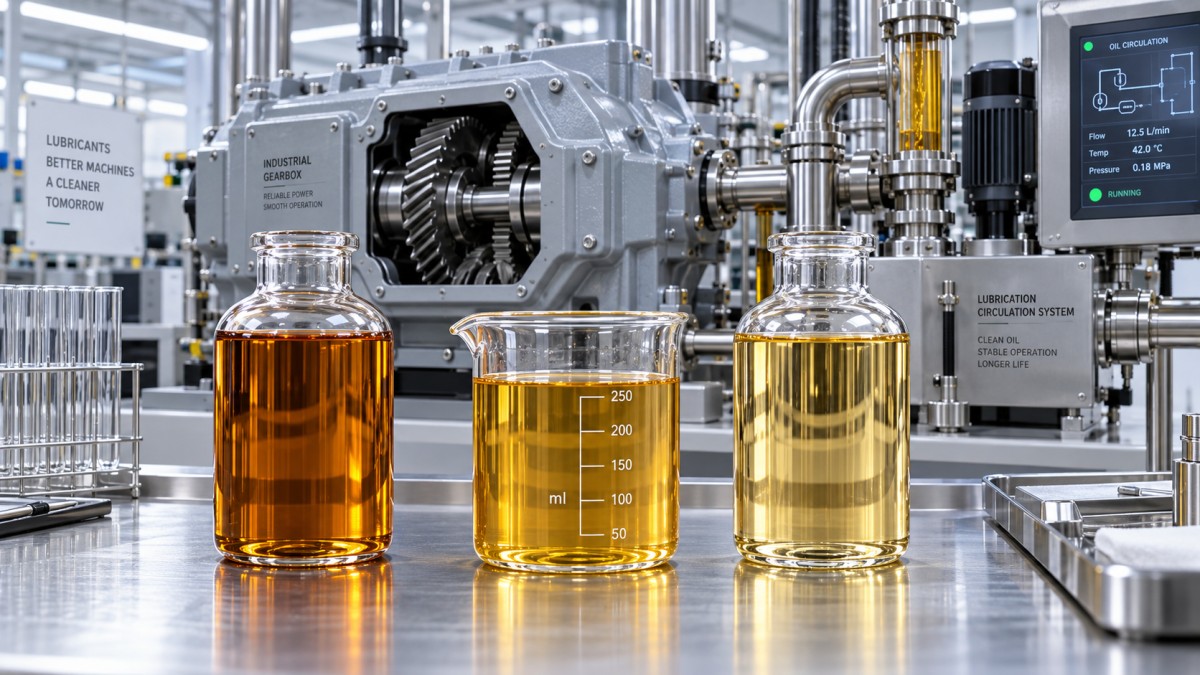
PAO-based lubricants are often the least problematic synthetic category when mixed with conventional mineral oils, because PAOs are relatively non-polar and are commonly used in formulations designed to resemble mineral-oil behavior while improving low-temperature flow and oxidation stability. This does not mean every PAO lubricant is interchangeable with every mineral lubricant. The finished product may contain ester co-base oils, friction modifiers, extreme-pressure additives, detergents, dispersants, rust inhibitors, or other components that alter compatibility.
Synthetic esters require more caution. Many esters have high natural solvency and may blend physically with mineral oils or PAOs. However, their polarity can affect seal materials, water tolerance, additive balance, and deposit control. In some formulations, an ester is used only as a minor component to improve additive solubility or lubricity; in others, it is the principal base oil. Those are not equivalent situations.
PAG lubricants are the clearest example of why general assumptions are risky. Many PAGs are not compatible with mineral oils or PAOs. A mixture can become cloudy, separate, lose predictable viscosity behavior, create lubrication inconsistency, or affect deposits and seals. PAG gear lubricants, compressor oils, and specialty industrial fluids should therefore not be topped up with mineral oil unless the lubricant supplier explicitly approves the combination.
Other specialty synthetic fluids, including silicone fluids, phosphate esters, and certain refrigeration or process lubricants, should be treated as separate chemical systems. Their use is often linked to fire resistance, gas compatibility, temperature limits, process exposure, or regulatory requirements. Mixing them with mineral oils without formal confirmation can defeat the reason they were selected in the first place.
What can go wrong when two oils are mixed?
The most visible failure mode is separation or haze. A cloudy mixture may indicate poor solubility, water contamination, wax precipitation, or an additive incompatibility. Yet a clear blend should not be taken as proof that the mixture is safe. The more damaging effects may emerge only after the lubricant has circulated at operating temperature.
Viscosity can move outside the acceptable range. If two oils have different ISO viscosity grades, mixing changes the resulting viscosity. The final value is not always a simple arithmetic average, particularly across different base-oil chemistries. In hydrodynamic bearings, gears, hydraulic pumps, and compressors, a deviation in viscosity can reduce film thickness or increase fluid friction and heat generation. A higher-quality synthetic oil does not compensate for a viscosity grade that is wrong for the machine.
Additives can interfere with each other. Industrial lubricants are balanced systems. Antiwear chemistry, extreme-pressure additives, antioxidants, detergents, metal deactivators, antifoam agents, and corrosion inhibitors are selected to work together. Combining products may dilute a required additive concentration or destabilize a performance balance. This concern is especially relevant when mixing hydraulic oils, turbine oils, circulating oils, paper-machine oils, and lubricants used in systems with fine filtration or servo valves.
Water handling may change. Some lubricants are designed to shed water rapidly, while others disperse or tolerate limited water differently. A mixture that changes demulsibility can make it harder to remove water from reservoirs. In systems exposed to condensation, washdown, steam leakage, or humid conditions, that can accelerate corrosion and reduce bearing life.
Foam and air-release behavior may deteriorate. Foam is not merely a cosmetic issue. Persistent foam can lead to oxidation, poor pump performance, erratic hydraulic response, lubricant overflow, and reduced heat transfer. Entrained air is particularly problematic in hydraulic systems because it can contribute to noise, cavitation-like damage, and unstable actuator movement.
Seals and coatings may respond differently. Seal compatibility depends on the lubricant chemistry and the elastomer or polymer in contact with it. A blend can alter swell, hardness, shrinkage, or extraction behavior. The risk is not confined to shaft seals; it may also affect hoses, gasket materials, paints, reservoir coatings, and filter media.
Does a small top-up amount matter?
It can. The acceptable contamination level depends on the system volume, lubricant type, asset criticality, operating temperature, and the reason for the synthetic lubricant’s use.
In a large industrial gearbox holding several hundred liters, a small quantity of a compatible mineral oil may have limited immediate effect. In a compact hydraulic power unit, oil-injected screw compressor, high-speed spindle, or precision circulation system, the same amount may represent a meaningful percentage of total fill volume. A small addition can also be significant where the lubricant is specified for food-contact incidental exposure, fire resistance, biodegradability, low-temperature performance, or compatibility with a refrigerant or process gas.
The question is not only “Will the machine keep running?” It is whether the mixed lubricant still complies with the equipment specification and whether its remaining service life can be predicted with confidence. An unplanned top-up may avoid immediate downtime while creating uncertainty about oil-change timing, warranty obligations, contamination history, and root-cause analysis if a later failure occurs.
Mixing during changeover is different from topping up
A complete oil change rarely removes every trace of the previous lubricant. Residual fluid remains in lines, coolers, filter housings, pumps, valves, bearing housings, and low points in the system. This is normal, but it must be accounted for when changing from mineral oil to a synthetic product or between synthetic chemistries.
Where compatibility is confirmed, residual oil may be acceptable within the lubricant supplier’s stated limit. Where it is not confirmed, a controlled conversion is needed. Depending on the equipment and product pair, this can involve draining at operating temperature, replacing filters, cleaning reservoirs, flushing with an approved fluid, cycling the system, draining again, and refilling with the target lubricant. Some applications require dismantling or targeted cleaning because trapped old oil cannot be reduced adequately through draining alone.
Flushing should not be improvised with solvents, diesel, or a random low-cost oil. Such practices can reduce residual contamination temporarily while introducing poor lubricity, seal damage, fire risk, or residues that affect the new lubricant. The appropriate procedure should come from the equipment manufacturer and the lubricant supplier, particularly for critical machinery.
How to assess compatibility before combining oils
Start with the product data, not the marketing category. Identify the exact product names, viscosity grades, base-oil type where disclosed, intended application, and current equipment specification. Safety data sheets can help identify broad compositional characteristics, but they often do not provide enough detail to approve a mixture. The most reliable source is a written compatibility statement from the lubricant manufacturer or its technical service organization.
Several questions should be resolved before any planned mixing:
- Does the equipment manufacturer permit the proposed lubricant type and viscosity grade?
- Are both products intended for the same application, such as hydraulic service, gear service, compressor service, or turbine service?
- Are the base-oil families compatible at the expected temperature range?
- Does either product carry a special approval, food-grade designation, fire-resistant classification, biodegradable claim, or process-specific requirement that blending could compromise?
- What residual percentage of the old oil is acceptable during conversion?
- Will the mixture affect filters, seals, paint, yellow metals, or water-separation requirements?
For high-value or safety-sensitive assets, supplier guidance may be supplemented by laboratory evaluation. A simple bench blend can reveal gross separation, haze, sediment, or abnormal viscosity change, but it cannot replicate long-term oxidation, shear, contamination, or component interactions. Laboratory oil analysis is useful for measuring viscosity, water, particle contamination, acidity-related indicators, elemental trends, and oxidation condition. It is not, by itself, proof that two products are chemically or operationally compatible.
Situations where mixing should generally be avoided
There are applications in which the burden of proof should be high. Avoid unapproved mixing in fire-resistant hydraulic systems, refrigeration compressors, oxygen-service equipment, food-processing machinery, wind turbine gearboxes, turbines, high-speed spindles, heavily loaded industrial gear drives, systems with servo or proportional valves, and machinery operating under an OEM lubricant approval program.
Specialty PAG lubricants also warrant a strict no-assumption approach. The same applies when changing to or from a lubricant selected for a particular refrigerant, gas process, elastomer package, or environmental requirement. In these cases, a modest purchase saving from using available stock can be outweighed by the cost of flushing, unplanned maintenance, component damage, rejected production, or lost warranty support.
What to do after accidental mixing
Do not automatically drain a system solely because a small amount of another oil entered it, but do not ignore the event. Record the products, estimated quantity, reservoir capacity, equipment identification, date, and operating condition. This information allows the mixture ratio to be estimated and provides an auditable maintenance history.
Obtain written technical advice using those details. If the products are incompatible or the contamination level is outside the supplier’s limit, plan a controlled drain and conversion rather than allowing the mixture to remain until the next routine interval. If continued operation is approved, establish an earlier inspection and oil-analysis point appropriate to the asset’s duty. Watch for changes in appearance, foam, reservoir level, filter differential pressure, operating temperature, leakage, vibration, and abnormal noise, while recognizing that the absence of visible symptoms does not prove the mixture is harmless.
The practical decision
Synthetic lubricants can be mixed with mineral oils in some cases, especially where a PAO-based product and a comparable mineral-oil formulation are involved. But compatibility must be demonstrated for the finished lubricants, not presumed from generic labels. The right decision depends on chemistry, viscosity, additive system, component materials, operating environment, residual-fluid volume, and OEM requirements.
Where approval is unavailable, maintaining lubricant identity is the safer operating discipline: use dedicated transfer equipment, label containers clearly, control top-up points, and avoid substituting oil based only on viscosity grade or the word “synthetic.” In lubrication management, preventing an unverified mixture is usually less costly than trying to establish its consequences after it has entered a working system.
Recommended News
 How CNC controller cycle time speed affects machining throughputCNC controller cycle time speed can raise machining throughput by sustaining feed rates on complex toolpaths. Learn how to optimize CAM, look-ahead, and machine dynamics.
 When a 4 axis vertical machining center is the better fit than 3-axisDiscover when a 4 axis vertical machining center outperforms 3-axis machining—reduce setups, improve datum control, and boost efficiency for complex multi-face parts.
 When industrial fasteners bolts need traceable material certificationIndustrial fasteners bolts need traceable material certification for critical applications. Learn what QA teams should verify to reduce risk and ensure compliance.
 How to size pump systems for cooling circuits for stable flow ratesPump systems for cooling circuits: learn how to match flow, total dynamic head, NPSH, and controls for reliable, energy-efficient cooling performance.
 When does software as a service reduce CNC data management costs?Software as a service can lower CNC data management costs by reducing IT overhead, manual reporting, and disconnected records. Discover when SaaS delivers measurable savings.
 CNC investment trends 2026: are automation upgrades taking priority?CNC investment trends 2026 reveal why automation upgrades are reshaping capacity plans. Compare robots, pallet systems, and new machines for smarter CNC growth.
 How to size high pressure pumps for stable chemical injection ratesHigh pressure pumps sizing guide for stable chemical injection rates—learn how to balance flow range, pressure, suction conditions, materials, and controls for reliable dosing.
 When organic chemicals are suitable feedstocks for synthetic lubricantsOrganic chemicals can unlock high-performance synthetic lubricants. Learn how purity, stability, compatibility, and supply control shape reliable industrial formulations.
 What machine tool market size reveals about capital spending cyclesMachine tool market size reveals capital spending cycles through order mix, automation, replacement demand, and capacity signals. Discover what drives smarter investment decisions.
 What causes solar inverters to trip repeatedly after installationSolar inverters tripping repeatedly? Discover key causes, from grid voltage and DC faults to wiring, settings, heat, and practical troubleshooting steps.
 How a tool life calculation chart improves cutting parameter decisionsTool life calculation chart insights help optimize cutting speed, feed, and depth for predictable tool changes, better part quality, and lower machining costs.
 What to check before choosing an industrial lubricating oils factoryIndustrial lubricating oils factory selection guide: compare quality control, formulation fit, traceability, technical support, and total cost to reduce downtime risks.
 Where machine shop digital transformation delivers the fastest paybackMachine shop digital transformation delivers faster payback by reducing downtime, setup delays, quality risks, and capacity constraints with focused, measurable workflows.
 When a semiconductor manufacturing solutions provider can shorten process ramp-upA semiconductor manufacturing solutions provider can shorten ramp-up through validated hardware, change control, field support, and resilient supply chains.
 How to evaluate CNC tooling suppliers in Europe for repeatable precisionCNC tooling Europe: learn how to evaluate suppliers for repeatable precision, stable tool life, application support, traceability, and resilient delivery.
 When does manufacturing competitiveness consulting pay off for a plant?Manufacturing competitiveness consulting pays off when plants face costly constraints, capital decisions, quality risks, or supply disruptions. Learn how to build a measurable ROI case.
 How to order acoustic ceiling tiles in bulk without overbuyingAcoustic ceiling tiles bulk buying made simple: calculate accurate quantities, control waste, secure spare stock, and plan phased deliveries to avoid costly overordering.
 Which laboratory microscopes fit routine quality inspection work?Laboratory microscopes for routine quality inspection: compare stereo, digital, compound, and measuring options to improve defect detection, documentation, and throughput.
 Can AI for multi axis machining reduce errors in complex toolpaths?AI for multi axis machining helps reduce complex toolpath errors through smarter collision detection, kinematic analysis, post validation, and machine-data insights. Learn how to improve precision.
 How seamless steel pipes are checked for wall-thickness consistencySeamlesssteelpipes wall-thickness checks explained: learn how ultrasonic scanning, calibration, and tolerance control ensure reliable, pressure-ready pipe quality.
 When a horizontal boring machine for metalworking improves large-part setupHorizontal boring machine for metalworking: learn how stable datums, rotary indexing, and rigid fixturing improve large-part accuracy and setup efficiency.
Search News
Popular Tags