When integrated precision manufacturing solutions reduce launch delays
When Integrated Precision Manufacturing Solutions Reduce Launch Delays
Launch delays rarely begin at commissioning. They usually take shape much earlier, when an apparently minor mismatch moves quietly across design, sourcing, fabrication, assembly, and testing. A machined housing may meet its drawing dimensions but fail to account for seal compression. A pump package may be selected for pressure and flow while overlooking fluid compatibility, pulsation, or service access. A die-cast component may be economical in volume, yet its porosity assumptions were never aligned with the later machining or leak-test requirement.
By the time these issues appear on the shop floor or at site acceptance, the critical path is already under pressure. Replacement materials have longer lead times, engineering changes require renewed approvals, and field teams are asked to solve problems that should have been resolved during design release. The practical value of integrated precision manufacturing solutions is not simply that more components come from a coordinated supply base. It is that technical decisions are connected before they become schedule problems.
For complex industrial programs, integration links CNC machining and tooling with fastening and sealing, fluid control, die-casting and mold engineering, and the lubricants or functional chemicals that support production and operation. It creates a common engineering language around interfaces, material condition, inspection evidence, traceability, and delivery readiness. That discipline does not eliminate every late change. It does make late changes more visible, more contained, and less likely to derail a launch.
The real source of delay is often the interface
Most industrial schedules are built around major milestones: design freeze, long-lead procurement, fabrication, factory acceptance, installation, and ramp-up. Yet the risks that disturb those milestones often sit between disciplines. A drawing can be technically complete for a machining supplier while still leaving open questions for the assembly engineer. A material specification can identify a grade but omit heat-treatment condition, surface finish, cleanliness, coating restrictions, or documentation requirements. Each omission invites interpretation.
Precision components magnify this problem. Tight tolerances are not automatically evidence of a robust design; they may introduce unnecessary processing steps, measurement burdens, scrap exposure, and capacity constraints. Conversely, a tolerance that looks reasonable in isolation may fail once geometric stack-up, thermal expansion, bolt preload, vibration, or operating media are considered. The right question is not whether every component is manufactured precisely. It is whether the assembled system performs reliably under its actual operating conditions.
This is particularly relevant where high-performance assets combine structural parts, rotating equipment, hydraulic or chemical circuits, and controlled joining methods. A sealing decision can affect machining roughness requirements. A lubricant choice can affect elastomer compatibility and contamination control. Tooling strategy can influence how rapidly a design modification can be absorbed without compromising repeatability. Treating these items as separate procurement categories may be administratively convenient, but it can create engineering blind spots.
What integration changes before production starts
A well-structured integrated approach begins before the purchase order reaches the machine shop. It brings manufacturing, quality, procurement, and package engineering into the same review of the critical interfaces. The aim is not to turn every review into a lengthy committee exercise. It is to identify the few decisions that could stop assembly, delay verification, or create unacceptable operational risk.
The first useful output is a shared definition of what is genuinely critical. This normally goes beyond nominal dimensions. It can include datum strategy, thread and fastener standards, allowable surface defects, sealing faces, pressure boundaries, corrosion exposure, cleanliness levels, material certificates, nondestructive examination requirements where applicable, and the inspection method used to demonstrate conformance. International references such as ISO, DIN, ASME, and JIS may be relevant, but naming a standard alone is not enough. The applicable edition, project specification, acceptance criterion, and contractual hierarchy still need to be clear.
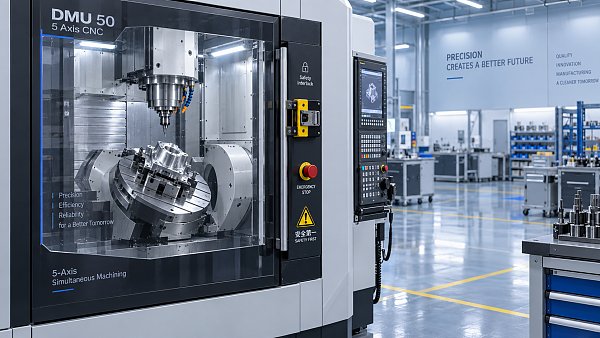
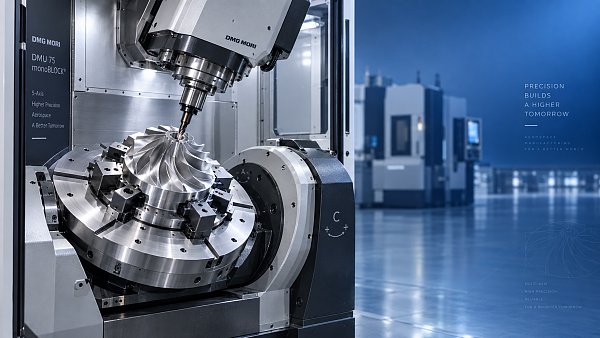
The second output is a manufacturing route that reflects function rather than merely part geometry. A five-axis machining center may reduce setups for complex parts, but that does not resolve fixturing stability, tool access, heat distortion, burr control, or measurement strategy. Die casting may reduce secondary operations for suitable components, yet it demands early decisions on tooling, alloy behavior, wall thickness, and the consequences of any later design change. A credible route identifies these constraints while there is still time to act.
The third output is a controlled evidence package. Depending on project requirements, this can include material traceability, dimensional inspection records, process approvals, test reports, coating records, and nonconformance handling. The objective is not paperwork for its own sake. It is to prevent a completed part from being held at final inspection because the evidence needed for release was never defined.
A practical view across the manufacturing chain
The following decision areas frequently deserve joint review because a change in one area can alter cost, lead time, and operational reliability elsewhere.
These checks are not a substitute for specialist design authority. They help the design authority receive earlier and better questions from the manufacturing chain. That distinction matters. Integration should preserve accountability while reducing the gaps between teams that hold different pieces of the technical picture.
Why supply-chain intelligence belongs in technical planning
Engineering release cannot be separated entirely from commercial reality. Material availability, qualified processing capacity, tooling lead time, and logistics exposure all influence the feasibility of a launch plan. This does not mean changing specifications whenever prices move. It means knowing which parts of the bill of materials are vulnerable enough to require alternatives, early reservations, or an additional review.
Steel, titanium, and synthetic base oils, for example, may be exposed to different market conditions and supplier networks. The relevant risk is not only price. It can be mill lead time, heat-lot traceability, regional processing capacity, export constraints, or an inability to obtain a required material condition in the needed quantity. For a project team, the most useful signal is not a broad statement that supply chains are uncertain. It is a component-level view of where substitution is technically possible, where it is not, and what approval path would be needed if an alternative becomes necessary.
This is one reason technical intelligence platforms such as Global Precision-Machining & Engineering (G-PME) are relevant to launch planning. G-PME’s framework spans advanced CNC machining and tooling, fastening and sealing systems, specialized fluid control and pumps, precision die-casting and mold engineering, and industrial lubricants and functional chemicals. Its value lies in connecting performance protocols and standards-based comparison with procurement and supply-resilience questions. A project team still needs to validate its own drawings, specifications, and contractual requirements, but cross-sector visibility can reveal dependencies that a single-category sourcing process may overlook.
Avoid the false comfort of a design freeze
A released drawing is often treated as the end of uncertainty. In reality, it may only mark the point at which uncertainty becomes more expensive. A design freeze is reliable only when the design has been tested against manufacturing capability, inspection practicality, assembly sequence, maintenance access, and supply availability. If those checks have not happened, the project may have frozen assumptions rather than resolved them.
One recurring mistake is to push all discussion of manufacturability downstream to protect the design schedule. This can create an illusion of progress, especially where procurement activity is measured by order placement rather than by readiness for production. Another is to request supplier feedback without defining which feedback can alter the design and who has authority to decide. The result is a stream of comments that arrives late, conflicts across suppliers, and is difficult to convert into controlled action.
A better approach is to create a short list of release gates for critical items. Before release, teams should be able to answer: Is the material state fully defined? Are the functional surfaces and their inspection methods clear? Is there an agreed path for deviations? Have sealing, fastening, and fluid-contacting materials been reviewed as a system? Does the production route depend on tooling or specialist processes with meaningful lead times? Which documents must accompany the item at inspection or handover?
Not every item needs the same level of scrutiny. Applying heavy controls to simple, noncritical parts can slow a program without reducing meaningful risk. The discipline is to focus on components that affect safety, pressure containment, alignment, precision motion, contamination control, or the commissioning sequence. Those are the parts most likely to convert a small discrepancy into a launch delay.
Building a launch-ready manufacturing plan
The strongest plans do not treat quality, schedule, and supply as competing agendas. They make their trade-offs visible. A slightly longer lead time for a verified material route may be preferable to a faster route that leaves documentation or performance questions unresolved. A modular design change may be worth accepting if it prevents a larger tooling revision. A second source can improve resilience, but only if the critical characteristics, test methods, and change-control rules are aligned across both sources.
For project leaders, the practical next step is to review the critical path through the lens of interfaces rather than purchase orders. Map each critical component to its material source, manufacturing route, joining or sealing requirement, test evidence, and installation dependency. Then identify where one unresolved assumption can block several downstream activities. That map often provides a more honest picture of launch readiness than a schedule populated only with nominal delivery dates.
Integrated precision manufacturing solutions reduce delays when they are used as a decision framework, not a broad sourcing slogan. The most useful outcome is straightforward: fewer surprises at assembly, faster resolution when variation occurs, and a clearer basis for deciding what must be confirmed before the project reaches the point where time is hardest to recover.
Recommended News
 Choosing carbide end mills for stainless steel without edge chippingCarbide end mills for stainless steel: learn how to prevent edge chipping with the right substrate, geometry, coating, coolant, and stable milling parameters.
 What contract manufacturing support should cover before sourcingIndustrial procurement support for contract manufacturing: learn what to verify before sourcing, from DFM and traceability to quality, capacity, cost control, and compliance.
 When integrated precision manufacturing solutions reduce launch delaysIntegrated precision manufacturing solutions help industrial teams prevent launch delays by aligning design, sourcing, machining, sealing, testing, and supply-chain readiness.
 When a horizontal boring machine improves accuracy in large metal partsDiscover when a horizontal boring machine for metalworking improves accuracy in large parts, protecting critical bore alignment, stable datums, and assembly-ready results.
 What to verify before choosing a fluid control supplier for critical flowChoose a fluid control supplier with confidence: verify pressure cycling, material compatibility, flow validation, traceability, sealing, and long-term support for critical applications.
 Cleanroom equipment application guidance to reduce contamination riskIndustrial application guidance for cleanroom equipment: reduce contamination risk with practical airflow, material flow, maintenance, and process protection strategies.
 When should wind turbine parts be replaced instead of repaired?Wind turbine parts: learn when replacement is safer than repair, how to reduce repeat failures, protect uptime, and make smarter maintenance decisions.
 What to verify before choosing a coolant flow rate and pressure supplierCoolant flow rate and pressure supplier selection guide: verify duty points, pump curves, filtration, controls and service support for reliable machining performance.
 How mold design choices affect cooling time in injection moldingDiscover how mold design affects injection molding cooling time, part stability, cycle efficiency, and long-term production quality with practical engineering insights.
 Machine tool standards alerts that require 5-axis safety procedure updatesMachine tool standards alerts can trigger critical 5-axis safety procedure updates. Learn which changes demand action to protect operators, equipment, and production uptime.
 Does manufacturing standards compliance for semiconductors affect EDM tool approval?Manufacturing standards compliance for semiconductors shapes EDM tool approval through traceability, validation, contamination control, and inspection. Learn what proves reliable capability.
 Which medical grade materials withstand repeated sterilization in pumps?Medical grade materials for sterilizable pumps: compare 316L, PEEK, PPSU, PTFE, silicone, and EPDM for steam, radiation, and chemical resistance.
 What G-code compatibility issues arise when moving to 5-axis centers?G code compatibility issues in 5-axis centers can affect TCP, rotary limits, feeds, and safety. Learn how to validate programs before production.
 Can custom mailer boxes reduce damage costs in subscription shipping?Custommailerboxes can lower subscription shipping damage costs through right-sizing, protective inserts, stronger materials, and efficient pack-out. Discover how to reduce claims and improve delivery performance.
 How to assess a lubricants manufacturer's batch traceabilityLubricants manufacturer batch traceability: learn how to audit records, controls, CoAs, packaging, and recall readiness to reduce supply risk and protect uptime.
 When solar inverters should be replaced instead of repairedSolar inverters: learn when recurring faults, obsolete parts, safety damage, and rising lifecycle costs make replacement smarter than repair.
 What to verify before choosing a first aid kits distributorFirst aid kits distributor checklist: verify compliance, traceability, expiry control, replenishment, and multi-site delivery before choosing a reliable supplier.
 How mold engineering design reduces warpage in thin-wall partsMold engineering design reduces thin-wall part warpage through balanced gating, cooling, packing, and ejection for stable, production-ready precision.
 What to audit at a CNC machine tools factory before approving a supplierCNC machine tools factory audit guide: verify machining accuracy, metrology, traceability, workforce skills, and capacity resilience before approving a precision supplier.
 When does a horizontal boring machine with ATC justify its cost?Discover when a horizontal boring machine with ATC delivers ROI through faster setups, higher uptime, lower labor costs, and reliable capacity growth.
 How office acoustics affect speech privacy in open-plan workspacesOffice acoustics shape speech privacy in open-plan workspaces. Discover practical strategies for reducing distractions, protecting sensitive conversations, and improving focus.
Search News
Popular Tags