
How coating thickness affects carbide tool coating costs
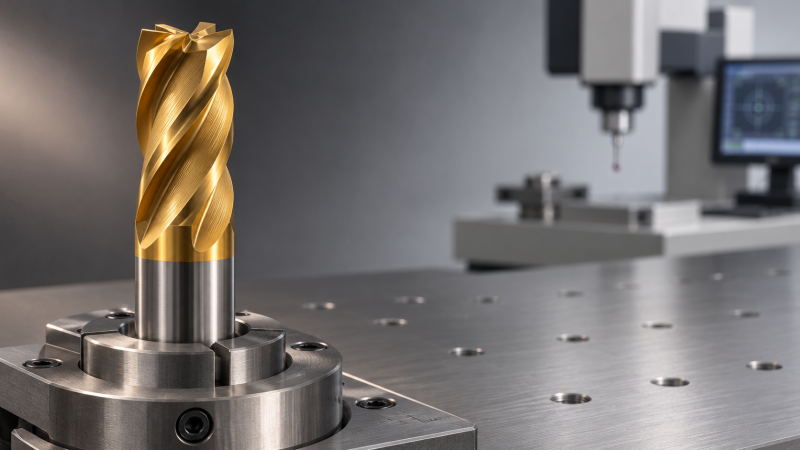
A thicker coating can increase the price of a carbide cutting tool, but it does not automatically reduce machining costs. Additional deposition time, coating material and processing constraints can raise the supplier’s cost; the purchase is justified only when the coating produces enough useful tool life or other measurable production savings to cover the premium.
The decision becomes difficult when two quotations describe similar carbide tools but specify different coating thicknesses. A proper carbide coating cost analysis separates the price of the coating from its effect on wear, edge condition, cycle time and replacement frequency. Thickness should be compared alongside coating composition, deposition method and tool geometry—not treated as an independent measure of quality.
Where thickness enters the quoted price
Depositing more coating generally requires more processing time or a different production recipe, although the relationship is not necessarily proportional. A supplier may need to adjust deposition conditions, part positioning or batch loading to achieve a specified thickness and acceptable uniformity. Those changes can affect chamber utilization and the number of tools processed in a run.
Coating material is another input, but it may not be the dominant cost. Cleaning, surface preparation, handling, masking, inspection and post-treatment can remain necessary regardless of thickness. A thicker specification can also introduce additional inspection or rejection risk if the required range is difficult to achieve on the tool’s geometry.
For a newly purchased coated tool, the coating charge may be embedded in the unit price. For a recoating service, it may appear as a separate line item alongside stripping, edge preparation and transport. Ask suppliers to identify which services are included before attributing the entire difference between quotations to thickness.
Volume matters as well. Setup and handling charges may be distributed differently across a batch, while small or urgent orders can carry minimum charges. Comparing a large standard batch with a small custom batch does not isolate the economic effect of a thicker coating.
Thickness is useful only when it addresses the wear mechanism
A coating provides a functional surface over the carbide substrate. Depending on its composition and the cutting conditions, it may help resist abrasion, reduce chemical interaction or protect the tool from heat. More thickness can provide additional material before the substrate is exposed, but the extra layer also changes the cutting edge and the stresses within the coating.
On an application where gradual flank wear determines tool replacement, a thicker coating may be worth testing if the coating system adheres well and the edge remains sufficiently sharp. The potential saving comes from machining more acceptable parts before each replacement, not from thickness itself.
The same increase may be counterproductive on a sharp finishing tool. Coating can alter edge radius and surface texture, affecting cutting forces, surface finish or dimensional control. In interrupted cutting, a coating that performs well in steady wear may instead be limited by chipping or delamination. Extra thickness does not necessarily prevent those failure modes and can, in some combinations of coating and substrate, make them more important.
Material buildup on the cutting edge is another separate issue. A coating’s chemistry and surface condition may influence adhesion of workpiece material, but buying a thicker version of the wrong coating is not a reliable remedy. Before paying for more coating, establish whether the tool is being retired because of gradual wear, edge fracture, buildup, finish deterioration or a preset production rule.
Make thickness specifications comparable
A nominal thickness on a quotation is not enough to establish that two offers are equivalent. Coating thickness can vary across the tool: the flank, rake face, cutting edge and deep features may not receive the same deposit. Geometry, fixturing and deposition process all influence distribution.
Request the following information in the same format from each supplier:
- Coating system: composition or grade, layer structure and deposition method, as well as the carbide grade and tool geometry.
- Thickness requirement: nominal value or range, measurement location and whether the stated value applies to a representative surface or a critical cutting area.
- Verification: measurement method, sampling approach and how nonconforming results are handled.
- Edge condition: preparation before coating, any post-coating treatment and the dimensional features that must remain within tolerance.
- Commercial scope: unit price, batch quantity, setup charges, lead time, delivery terms and any separate stripping or inspection charges.
Thickness measurement itself deserves attention because direct measurement on a small, curved cutting edge can be difficult. A supplier may measure a witness sample or an accessible surface rather than the edge that controls performance. That can be a practical quality-control method, but the relationship between the reported result and the critical tool surface should be understood. Do not compare values from different locations or methods as though they were interchangeable.
A narrow tolerance can also cost more than a wider one, even at the same nominal thickness. Specify a range that protects the application rather than demanding unnecessary precision. Where edge geometry is critical, a maximum thickness or a requirement for the finished edge condition may be as commercially relevant as a minimum coating thickness.
Convert the premium into cost per acceptable part
The simplest useful comparison starts with tool cost per acceptable part. Divide the delivered cost of each tool by the number of acceptable parts produced during its usable life. For an insert with multiple usable edges, use a consistent basis: cost per insert divided by total acceptable output from all usable edges, or cost per edge divided by output per edge.
Tool cost per acceptable part = delivered tool cost ÷ acceptable parts produced during useful life.
The thicker coating has a direct tool-cost advantage when its increase in acceptable output is proportionally greater than its increase in delivered tool cost. This is a threshold, not a prediction: a higher purchase price requires a correspondingly higher verified output merely to break even on tool spend. A tool that lasts longer in cutting time but produces more rejected parts may not meet that threshold.
Delivered cost should include the purchase or coating price and any incremental freight, handling or inspection cost attributable to the option. Keep common costs out of a comparison unless they change between alternatives. If a premium coating changes the number of tools held in inventory or the frequency of expedited orders, record those effects separately rather than hiding them in an assumed unit price.
Include changeovers and quality where they differ
Longer tool life can reduce replacement frequency. The economic value depends on whether a replacement actually interrupts a constrained machine, can be performed during planned downtime or occurs while another operation is running. Count the additional downtime attributable to the tool change, then apply the production’s agreed cost basis. Avoid treating every minute of scheduled machine time as lost revenue.
Quality effects can be material. A coating that maintains finish or dimensions for longer may reduce inspection intervention or scrap; one that fails unpredictably may create the opposite result. Include rework, scrap and extra inspection only when they can be linked to the tool option and measured consistently. Do not count the same rejected part both as reduced acceptable output and again as a full loss without defining which costs are included in each calculation.
Speed changes require separate treatment. If the thicker coating is tested at a higher cutting speed, any gain or loss reflects a combined tool-and-process change. That may be commercially useful, but it does not establish the effect of thickness alone. Compare both the current operating conditions and any proposed revised conditions before approving the purchase.
Set up a trial that supports a buying decision
A controlled trial should begin with a baseline: the current tool specification, its delivered cost, the operation, the replacement criterion and recent results under comparable conditions. Record workpiece material and condition, coolant or lubrication, machine setup, cutting parameters and the features used to accept the finished part. These variables can affect wear enough to obscure a coating comparison.
Where practical, change only the coating thickness while keeping the substrate, coating system, edge preparation and tool geometry the same. Confirm with the supplier whether a different thickness requires a different recipe or post-treatment; if it does, document that the trial compares complete tool options rather than thickness alone.
Run each option to the same defined endpoint. The endpoint might be a specified wear limit, loss of dimensional control, unacceptable finish or another agreed condition. A fixed replacement interval can be used when required by production, but it may prevent the test from revealing whether either tool has additional usable life. Do not extend an interval beyond established process controls merely to complete a cost comparison.
Record acceptable parts per edge, failure mode, actual changeover time and any quality interventions. Use more than a single edge where production allows, because variation between edges, workpiece batches and setups can distort an individual result. If the result is close to the break-even threshold or failures are inconsistent, the evidence may support a longer evaluation rather than an immediate specification change.
Use the result to write the purchase requirement
When a thicker coating lowers verified cost per acceptable part without unacceptable quality or reliability trade-offs, define the approved coating system, thickness range, measurement location and relevant edge requirements in the purchase specification. Preserve the trial’s operating conditions and replacement criterion with the approval so that a later process change does not silently invalidate the comparison.
When the premium does not break even, retain the less expensive option or investigate the limiting failure mechanism before requesting more coating. A thicker layer is a weak purchase requirement if tools are being replaced because of chipping, unstable dimensions or a fixed schedule unrelated to coating wear. In those cases, the next comparison may need to focus on edge preparation, geometry, coating system or process conditions instead.
Finally, review quotation changes against the approved specification. A lower price obtained by changing the measurement location, reducing preparation or substituting a different coating is not necessarily a saving on the same tool. Equally, an added charge for tighter thickness control should be accepted only when the controlled feature has a demonstrated role in the operation.
Recommended News
 How coating thickness affects carbide tool coating costsCarbide coating cost analysis: discover how thickness affects tool prices, wear and cost per part, and learn when a premium coating is worth the investment.
 What pressure stability data should a pump supplier provide?How do I shortlist the right high-pressure pumps supplier for stable pressure? Learn which test data to request and compare bids with confidence.
 How to evaluate an industrial supplier's delivery reliabilityStrengthen industrial procurement support and supplier evaluation with practical checks for delivery records, lead times, capacity, and recovery plans.
 Stonepeak Completes 65% Castrol Acquisition; Former Shell CEO to ChairStonepeak's 65% Castrol acquisition brings new leadership as former Shell CEO Ben van Beurden becomes chair. Explore potential implications for lubricant buyers and suppliers.
 How to inspect welded iron pipes for seam defectsInspect weldedironpipes for seam defects with a practical guide to visual checks, NDT methods, acceptance criteria, and safe repair decisions.
 How to assess electronics manufacturing solutions in North America for production capacityAssess electronics manufacturing solutions North America teams can rely on. Compare capacity, supply risks and quality controls to choose the right production partner.
 How to reduce thermal cracking in die casting mold insertsReduce thermal cracking in die casting mold inserts with practical tips on temperature control, cooling, steel selection and maintenance to extend tool life.
 Can portable telemedicine devices work with poor connectivity?Telemedicine hardware portable devices can support care with poor connectivity. Discover what works offline and how to evaluate reliable remote care workflows.
 How to choose rugs and carpets for high-traffic roomsDiscover how to choose rugs and carpets for high-traffic rooms. Compare materials, construction, cleaning needs, and fit to find a practical, lasting option.
 What affects the wholesale price of EPS sandwich panels?Compare EPS sandwich panels wholesale prices and discover how core density, steel facings, order size, and delivery costs affect your project budget.
 Japan's Machine Tool Export Controls Accelerate China's Five-Axis SubstitutionJapan's machine tool export controls are accelerating China's five-axis CNC substitution. Explore the implications for buyers and supply chains.
 Why do automatic mechanical watches stop when not worn?Why do automaticmechanicalwatches stop when unworn? Discover how power reserve works, how to restart your watch, and when to seek professional help.
 Choosing high-tensile bolts for industrial fastening in EuropeIndustrial fastening Europe: Learn how to select high-tensile bolts, coatings and standards for reliable joints, accurate preload and safer assembly.
 How does excess inventory affect fashion retail profitability?Discover how excess inventory erodes fashion retail profits through markdowns and holding costs, and learn practical ways to protect margins and free up cash.
 US Adds 50% Section 338 Tariff on Canadian Seals and Other ProductsUS Section 338 tariffs add 50% to covered Canadian seals, lubricants and other goods. Explore the potential impact on sourcing and supply chain costs.
 Can lean manufacturing reduce changeover time in injection molding?Discover how lean manufacturing can reduce injection molding changeover time with SMED, better preparation, standardized processes, and quality controls.
 How to estimate the payback period for a CNC machining centerEstimate your CNC machining center investment payback with a practical formula, installed cost checklist, cash-flow examples, and risk analysis.
 How cloud computing supports remote CNC machine monitoringDiscover how cloud computing enables remote CNC machine monitoring, from real-time alerts and troubleshooting to secure integration and smarter pilot decisions.
 LANXESS and BPCL to Explore Immersion Cooling Fluids and Advanced LubricantsLANXESS and BPCL are exploring immersion cooling fluids and advanced lubricants. Discover what the proposed collaboration could mean for buyers and suppliers.
 What OEM manufacturing support is needed for smart actuator testing?Explore OEM manufacturing support for smart devices: precision fixtures, firmware access, load testing, and traceable results. Learn what to demand for reliable smart actuator validation.
 How minimum order quantities affect wholesale bedding set costsBuying bedding sets wholesale? Discover how minimum order quantities affect unit prices, inventory risks, and total costs—and learn to negotiate smarter deals.
Search News
Popular Tags