How Can You Standardize Machining Specifications Across Suppliers?
A tight-tolerance component can pass inspection at one supplier and fail at another because the shops use different datum setups, surface-texture settings, or acceptance rules. The result is not just inconsistent inspection reports: parts may bind during assembly, require selective fitting, or trigger disputes over responsibility. Standardize the technical definition and verification method first, then qualify each supplier’s process against that same baseline. Requiring identical CNC machines is neither necessary nor sufficient.
The practical approach is to issue one controlled specification package covering drawing conventions, material condition, critical characteristics, measurement procedures, and change approval. Suppliers may use different manufacturing routes, but they must demonstrate conformity using comparable evidence. That distinction allows sourcing flexibility without letting each shop redefine what “acceptable” means.
Standardize acceptance, not every manufacturing choice
A purchase order that says “machine to drawing” leaves gaps when the drawing does not fully define inspection conditions or reference documents. Conversely, prescribing every cutter, fixture, and cutting parameter can lock suppliers into a process that does not suit their equipment. Separate requirements that affect interchangeability from production choices that suppliers can control.
Some applications need tighter process control. A thin-wall housing may depend on a defined stress-relief sequence; a sealing surface may prohibit particular finishing methods. Record those restrictions explicitly and explain their functional purpose. Do not turn supplier preferences into mandatory requirements without an engineering reason.
Resolve drawing interpretation before comparing quotations
Choose the governing dimensional and geometrical tolerancing system and specify its applicable edition. ASME Y14.5 and the ISO GPS framework are not interchangeable dictionaries. Their defaults and interpretation rules can differ, so mixing symbols and assumptions without clarification can change the acceptance boundary.
For an ISO-based package, identify the relevant GPS documents rather than simply writing “ISO tolerances.” These may include ISO 1101 for geometrical tolerancing, ISO 5459 for datums, and ISO 8015 for fundamental GPS rules. An ASME-based package should likewise identify the applicable requirements. Any supplementary interpretation must be explicit and consistent with the contractual baseline.
Datums deserve an engineering review before supplier release. A convenient inspection surface may not reproduce how the component locates in service. A mounting face, pilot diameter, and clocking feature may establish functional alignment more effectively than three easily accessible exterior surfaces. Specify datum targets or restraint conditions where necessary, particularly for flexible parts.
Also establish document precedence. State whether the drawing, annotated model, specification, or purchase-order attachment governs when information conflicts. Identify the authoritative model revision and units. A supplier should raise discrepancies before manufacture, not choose whichever document gives the easier tolerance.
Replace ambiguous notes with observable requirements
Notes such as “smooth finish,” “break all edges,” and “material equivalent allowed” invite different interpretations. Define surface texture with the required parameter and applicable measurement conditions; an Ra value alone may not describe the directional texture needed for a seal or sliding interface. Specify evaluation direction and filtering where these affect acceptance, using the selected surface-texture standard.
Define permitted edge breaks, burr limits, protected sharp edges, and inspection access. For materials, include grade, product form or condition where relevant, treatment requirements, and substitution approval. Chemistry alone does not establish equivalence when mechanical properties, residual stress, or corrosion performance matter.
Which CNC machine tool accuracy matters most for tight-tolerance parts?
The relevant accuracy is the one that controls the feature’s error budget under actual machining conditions. Linear positioning accuracy matters for feature locations across travel; repeatability matters for consistent returns to commanded positions. Neither proves that a finished part will meet tolerance after cutting forces, thermal drift, fixturing, and tool wear are included.
ISO 230-series machine tests can support equipment assessment, but they are not substitutes for part qualification. Ask what was measured, under which conditions, and how the result relates to the proposed work. A brochure accuracy figure may describe an unloaded machine at a favorable temperature rather than the operating condition relevant to your component.
Compare suppliers on demonstrated feature capability, not machine brand, axis count, or encoder resolution. A well-controlled three-axis process may outperform an unsuitable five-axis route for a particular feature. Conversely, reducing setups with multi-axis machining may improve feature relationships when transfer errors dominate.
Make inspection results genuinely comparable
Two CMM reports can disagree even when both programs appear to follow the drawing. Differences may come from datum construction, point distribution, filtering, fitting algorithms, or part restraint. A short measurement-method sheet for critical characteristics is often more useful than requesting a longer inspection report.
For each critical characteristic, define the feature identifier, datum alignment, measurement location or coverage, and any evaluation settings that materially affect the result. For form and profile, sparse probing can miss local deviations. For bores, different fitting methods may report different sizes; select the evaluation appropriate to the drawing requirement rather than allowing software defaults to decide.
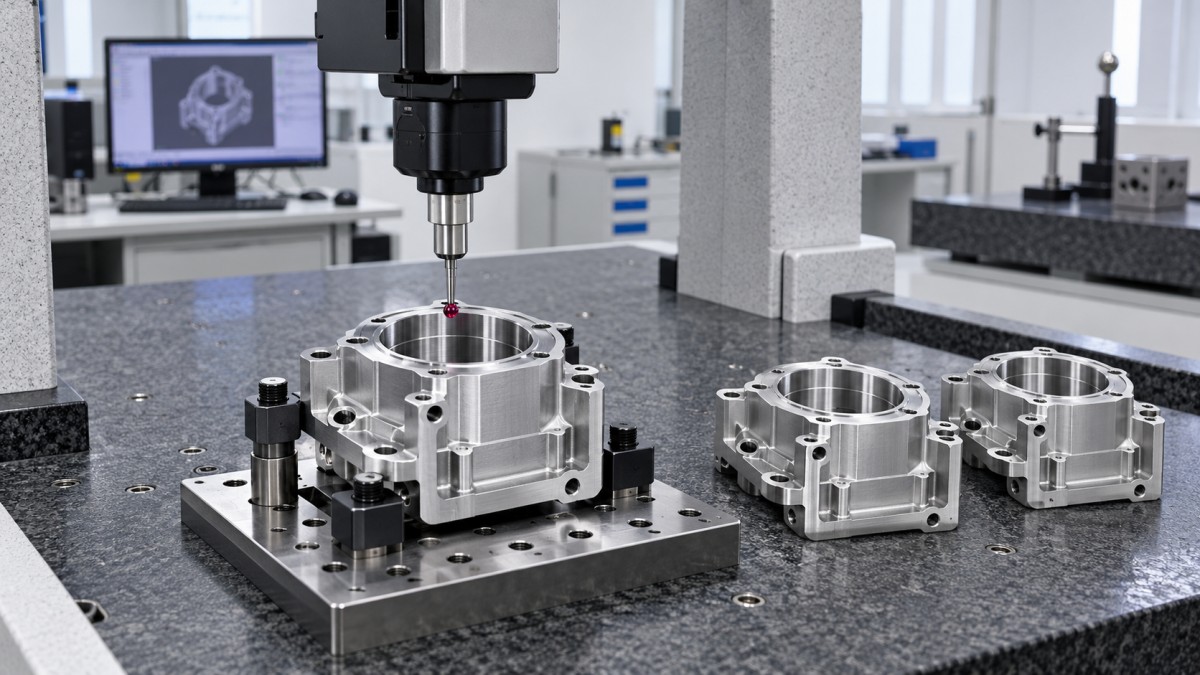
Specify the part’s inspection state: before or after coating, after heat treatment, restrained or unrestrained, and with any required stabilization. Dimensional specifications generally reference 20°C unless otherwise stated; actual measurements may require temperature control or validated compensation. Different materials, temperature gradients, and insufficient soaking time can undermine comparisons.
Resolution is not measurement uncertainty. Require a measurement method capable of supporting the tolerance and an agreed conformity decision rule. Where applicable, reference ISO 14253-1 or another agreed rule and document how uncertainty affects acceptance near a limit. Avoid inventing one universal equipment-to-tolerance ratio for every feature.
Before production approval, have suppliers and the receiving inspection team measure the same stable artifact or representative parts using agreed methods. Investigate disagreement before designating either result as definitive. For contact measurements, study repeatability and reproducibility with representative operators, fixtures, and geometry; include bias or method correlation where relevant.
Qualify the process without confusing samples with capability
A conforming first article shows that the submitted component meets the checked requirements. It does not establish that the process will remain stable across tool changes, setups, material lots, or operating temperatures. Keep first-article approval and production-capability approval distinct.
- Review feasibility before award. Require suppliers to identify exceptions, difficult characteristics, outsourced operations, and proposed inspection limitations against the same specification package.
- Approve a representative first article. Link each reported result to a drawing characteristic and retain material and treatment records. Include characteristics that cannot be checked after subsequent processing.
- Evaluate production variation. Obtain evidence covering the sources of variation that matter, rather than relying only on consecutive parts from one favorable setup.
- Agree ongoing controls. Define sampling, tool-life checks, reaction plans, and requalification triggers according to functional risk and demonstrated performance.
Capability indices such as Cp and Cpk require suitable data and a stable process; non-normal distributions need appropriate analysis. Set any contractual thresholds and study conditions before qualification. Do not compare one supplier’s short machine trial with another supplier’s long-term production data as though the indices describe the same conditions.
For low-volume work, conventional capability studies may be impractical. Use a documented combination of process qualification, setup verification, critical-feature inspection, and risk-based controls. Full inspection can screen measurable characteristics, but it does not automatically control hidden damage or an incapable measurement method.
Keep revisions and deviations from becoming competing specifications
Release the drawing, model, material requirements, inspection plan, and approved clarifications as one identifiable package. Each purchase order should reference that package revision. Require acknowledgment from the supplier and flow down applicable requirements to heat-treatment, coating, and other subcontractors.
A deviation approval should identify the affected characteristic, permitted departure, covered quantity or lots, and expiry or closure condition. It should not silently amend the master drawing. Record the disposition with shipment documentation so receiving inspection does not reject an authorized exception or accept it indefinitely.
Define which process changes require notification or renewed approval. Moving a critical feature to another machine, changing a fixture, altering treatment sequence, or transferring an outsourced operation can invalidate qualification evidence. Routine tool replacement within an approved control plan need not receive the same scrutiny as a manufacturing-route change.
Use supplier disagreements to locate the missing control
When results conflict, first confirm revision, units, processing state, datum alignment, and measurement settings. Then compare uncertainty and repeat the measurement using the agreed reference method. Recutting parts before resolving the disagreement can destroy evidence and introduce unnecessary variation.
Assign ownership clearly: engineering controls functional requirements, quality controls the agreed verification framework, and procurement ensures that the contractual package reaches every supplier. Close each dispute with a specific clarification, corrected method, or controlled deviation. If the same ambiguity returns on the next order, the specification package—not merely the supplier’s workmanship—still needs correction.
Recommended News
 Why do automatic mechanical watches stop when not worn?Why do automaticmechanicalwatches stop when unworn? Discover how power reserve works, how to restart your watch, and when to seek professional help.
 Choosing high-tensile bolts for industrial fastening in EuropeIndustrial fastening Europe: Learn how to select high-tensile bolts, coatings and standards for reliable joints, accurate preload and safer assembly.
 How does excess inventory affect fashion retail profitability?Discover how excess inventory erodes fashion retail profits through markdowns and holding costs, and learn practical ways to protect margins and free up cash.
 US Adds 50% Section 338 Tariff on Canadian Seals and Other ProductsUS Section 338 tariffs add 50% to covered Canadian seals, lubricants and other goods. Explore the potential impact on sourcing and supply chain costs.
 Can lean manufacturing reduce changeover time in injection molding?Discover how lean manufacturing can reduce injection molding changeover time with SMED, better preparation, standardized processes, and quality controls.
 How to estimate the payback period for a CNC machining centerEstimate your CNC machining center investment payback with a practical formula, installed cost checklist, cash-flow examples, and risk analysis.
 How cloud computing supports remote CNC machine monitoringDiscover how cloud computing enables remote CNC machine monitoring, from real-time alerts and troubleshooting to secure integration and smarter pilot decisions.
 LANXESS and BPCL to Explore Immersion Cooling Fluids and Advanced LubricantsLANXESS and BPCL are exploring immersion cooling fluids and advanced lubricants. Discover what the proposed collaboration could mean for buyers and suppliers.
 What OEM manufacturing support is needed for smart actuator testing?Explore OEM manufacturing support for smart devices: precision fixtures, firmware access, load testing, and traceable results. Learn what to demand for reliable smart actuator validation.
 How minimum order quantities affect wholesale bedding set costsBuying bedding sets wholesale? Discover how minimum order quantities affect unit prices, inventory risks, and total costs—and learn to negotiate smarter deals.
 What should mechanical seal technical specification documents include?Explore technical specification support documentation for mechanical seals, covering materials, drawings, standards, and testing to reduce risks and make confident supplier approval decisions.
 Shanghai Plan Targets Ultra-Precision Machining and Five-Axis Machine Tool UpgradesShanghai's ultra-precision machining and five-axis machine tool upgrade priorities could shape equipment investment. Explore potential opportunities and what buyers should verify.
 How global trade tariffs affect the landed cost of injection moldsDiscover how global trade tariffs affect injection mold landed costs. Compare duties, freight, and customs rules to avoid hidden expenses and make smarter sourcing decisions.
 How to qualify a catalyst manufacturer for synthetic oil productionQualify a catalysts manufacturer for synthetic oil production with practical checks for performance, batch quality, and scale-up. Learn how to reduce risk and select a reliable supplier.
 Are CNC spindle suppliers expanding local repair for five-axis machines?Explore cnc spindle supplier trends in local repair for five-axis machines. Learn how to verify repair capacity, compare exchange options, and choose support that reduces downtime.
 China’s Base Oil Imports Hit 2026 Low in September; Top Three Suppliers Account for 82.5%China’s base oil imports hit a 2026 low of 67,400 tonnes in September, with three origins accounting for 82.5%. Explore the data and implications for sourcing and supply risk.
 How to verify batch quality with an industrial lubricating oils exporterBuying from an industrial lubricating oils exporter? Learn how to verify batch test results, sampling, and traceability to reduce purchasing risks and protect equipment.
 How to set relubrication intervals for industrial maintenanceImprove industrial maintenance with smarter relubrication intervals. Learn how to balance bearing conditions, grease quantity, and monitoring to reduce downtime and avoid costly failures.
 How to spot misleading claims on eco-friendly baby productsShopping for ecofriendlybabyproducts? Learn to spot greenwashing, verify certifications, and assess material and disposal claims so you can choose with confidence.
 John Crane Signs Three-Year Agreement to Improve Phosphate Mine Seal ReliabilityJohn Crane's three-year agreement targets phosphate mine seal reliability with on-site expertise and mechanical seal solutions. Explore its potential to reduce downtime.
 CNC Routing Plywood: Testing Tooling and Hold-Down TogetherExplore ZD1325 plywood routing capabilities by testing tooling and hold-down together. Learn how to assess edge quality, part retention, and repeatability before you invest.
Search News
Popular Tags