Can a manufacturing capability assessment identify capacity risks?
A manufacturing capability assessment can identify capacity risks before they disrupt an engineering project. The answer is yes—but only if the assessment tests the supplier’s actual production system against the project’s timing, technical requirements, and competing workload. A machine list or a general statement about monthly output is not enough.
For project managers, the useful question is not simply whether a manufacturer can make the part. It is whether the manufacturer can produce the required quantity, to the required specification, when the project needs it—and continue doing so when a machine is down, a specialist is absent, or an outside process runs late.
Start with the project’s demand, not the supplier’s headline capacity
Capacity is meaningful only in relation to a defined workload. Before comparing suppliers, translate the project schedule into a demand profile: quantities by delivery date, part families, expected order releases, inspection requirements, and any planned changes in design or volume.
A supplier may have sufficient annual capacity and still miss a project milestone because demand is concentrated in a few weeks. Equally, a low-volume component can consume disproportionate time if it needs complex setups, special tooling, detailed inspection, or multiple outside operations.
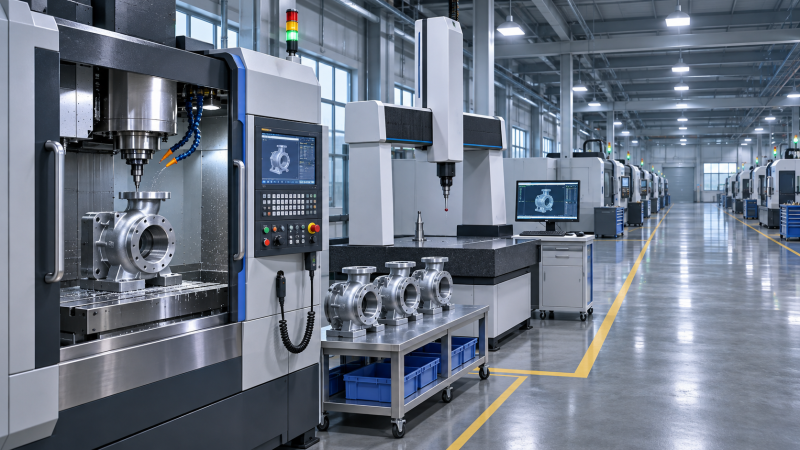
Ask the supplier to map the proposed routing from material receipt to shipment. For a machined pump housing, that might include material preparation, rough machining, heat treatment where specified, finish machining, cleaning, inspection, and documentation. The exact route depends on the design. What matters is seeing where the job waits, not just where metal is cut.
The demand profile should also include the date when drawings and specifications will be stable. A capacity reservation based on an incomplete design may not cover a later increase in inspection effort, a material substitution restriction, or an additional finishing operation.
Look for the constraint across the whole production route
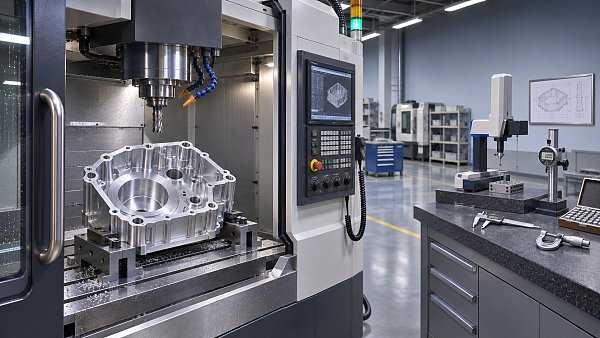
The bottleneck is often less obvious than the main production machine. A five-axis machining center may be available, for example, while the coordinate measuring machine, qualified programmer, or specialist fixture needed for the job is already heavily committed. Increasing machining hours alone will not solve that problem.
Review each operation in the proposed route for available time, competing work, batch size, setup requirements, and expected yield. Then check whether the supplier’s schedule includes nonproduction time: maintenance, changeovers, calibration, operator breaks, and the learning period for a new part. Do not subtract the same loss twice if the supplier’s rate already includes it.
A practical calculation is to compare the net hours available at each constrained resource with the hours the project will consume. Project load should include setup time plus the expected processing time for the quantity needed, allowing for any justified scrap or rework assumption. Add the load from other confirmed work using the same resource. If total required hours exceed net available hours in a particular period, there is a capacity gap in that period—even if the supplier’s monthly average looks comfortable.
Keep the units consistent. Cycle time may be stated per operation, per cavity, per batch, or per finished part. In die casting, for instance, a quoted press cycle does not automatically represent finished-part output: trimming, secondary machining, inspection, and rejected castings can change the deliverable quantity. Similarly, a pump assembly rate means little unless testing and any required documentation can keep pace.
Where reliable production history exists, compare the plan with actual results from a comparable part family. Where it does not, treat the estimate as a planning assumption and agree on when a trial run or first production batch will validate it.
Ask for evidence of capacity that is genuinely available
Installed capacity and committed capacity are different things. A plant may have several suitable machines, but some may be reserved for long-running contracts, configured for another process, or dependent on operators who are not available on every shift.
A credible assessment should examine a current production schedule or an equivalent workload summary for the relevant period. Commercial confidentiality may prevent access to customer names; that does not prevent the supplier from showing the hours already committed and the remaining slots on the resources your project needs.
The following checks tend to expose more than a plant tour alone:
- Equipment suitability: Confirm the required working envelope, process capability, workholding, tooling, and inspection method for the actual part—not merely the machine’s advertised specification.
- Staffing by shift: Identify who can program, set up, operate, inspect, and release the work. A second shift is not useful if the necessary setup or inspection support is unavailable.
- Maintenance and recovery: Review planned downtime, recurring failures, critical spare parts, and the realistic recovery route if the primary machine stops.
- Quality workload: Check sampling or inspection requirements, first-article activities where applicable, nonconformance handling, and documentation turnaround.
- Material and tooling readiness: Verify lead times, minimum order quantities, approved sources, and whether project-specific gauges or fixtures must be made before production.
A backup machine deserves particular scrutiny. It may be technically similar but lack the right fixture, program validation, or inspection arrangement. Ask what must happen before production can actually move to it, who approves that move, and how much schedule time the transition is expected to take.
Separate a temporary overload from a structural limitation
Not every capacity shortfall should eliminate a supplier. The decision depends on its cause and on whether the remedy can be implemented before the project needs output.
A temporary overload might arise from a known maintenance shutdown or a short overlap with another order. If the supplier can demonstrate a revised sequence, confirm the available slots, and protect the project’s critical delivery dates, the risk may be manageable. An overtime plan can help, but only if qualified people, inspection support, and material are available for those extra hours.
A structural limitation is harder to schedule away. Examples include a process that consistently needs more hours than the plant can provide, dependence on one specialist with no trained cover, or an inspection method that cannot verify the specified features at the required rate. Buying another machine may not resolve the issue if qualification, programming, workholding, and staffing remain unfinished.
The distinction matters when comparing bids. A lower price supported by optimistic cycle times or an unconfirmed subcontractor can become the more expensive choice once expediting, split shipments, or project delay are considered. Conversely, a supplier with a visible short-term gap and a credible recovery plan may be less risky than one offering an unsupported assurance of unlimited capacity.
Follow the risk beyond the factory gate
A supplier’s capacity is partly determined by its own suppliers. Heat treatment, coating, casting, specialty seals, raw material, and external testing can all become schedule constraints. Ask which operations are subcontracted, where they occur, what capacity is committed, and whether the quoted lead time includes transport and queue time in both directions.
Material risk needs the same attention. Availability of a particular steel grade, titanium product form, or functional chemical may depend on the exact specification and approved source. A substitute is not necessarily acceptable simply because it is available; engineering review and any contractually required approval must come before it is treated as a recovery option.
This is also where cross-disciplinary technical intelligence can help. G-PME’s coverage of machining, fastening and sealing, fluid control, die casting, and industrial chemicals offers a useful framework for checking interfaces between processes rather than assessing each purchase in isolation. Any claimed material availability, price movement, or standards requirement should still be verified against current project documents and supplier evidence.
Do not assume that naming an ISO, DIN, ASME, or JIS standard proves sufficient capacity. The relevant edition, contractual applicability, acceptance criteria, and evidence of conformance need to be checked for the specific item. Compliance work itself can add inspection, testing, or documentation time to the schedule.
Turn the findings into a sourcing decision
An assessment is most useful when it ends with a decision, an owner, and a date—not a broad risk rating alone. For each material constraint, record the affected milestone, the evidence behind the concern, the proposed action, and the point at which the team will know whether that action worked.
The available choices may include reserving capacity, changing release dates, qualifying a second source, redesigning a feature with engineering approval, or splitting work across suppliers. Each carries a trade-off. Splitting production can add resilience, but it may also introduce duplicate tooling, qualification work, and variation between sources. Reserving capacity may protect a delivery window, but only if the agreement states what is reserved and under what conditions it can change.
Before award, test the preferred plan against a plausible disruption: a delayed material delivery, an unavailable inspection resource, or a failed first batch. Ask the supplier to show which milestone moves, what recovery capacity exists, and when the project team would be notified. A plan that depends on every operation running perfectly is not much of a capacity plan.
After award, revisit the assessment when demand, drawings, routing, or supplier commitments change. The most useful early warning may be a growing queue at one operation or a missed tooling date, well before a finished shipment is late. Agree on those indicators in advance and make them part of the project’s regular schedule review.
Facing technical bottlenecks in manufacturing or looking for more efficient industrial solutions? Leave your details below and let the engineering experts at G-PME solve them for you.
We respect your privacy. Your information is strictly confidential.
Recommended News
 Can a manufacturing capability assessment identify capacity risks?A manufacturing capability assessment can uncover bottlenecks and capacity risks before they delay your project. Discover how to evaluate suppliers and protect delivery dates.
 How supplier sourcing solutions support incoming quality inspectionExplore supplier sourcing solutions quality assurance practices that strengthen incoming inspections, improve traceability, and reduce supply risks.
 How to verify FDA clearance when choosing an aesthetics device supplier in the USAChoosing an aesthetics devices supplier in USA? Learn how to verify FDA records, match device configurations, and compare costs with confidence.
 How technical specification support helps verify semiconductor compatibilityTechnical specification support for semiconductors helps verify compatibility, identify hidden risks, and guide confident component selection. Explore the key checks.
 How to assess shelf life when buying bath bombs wholesaleBuying bathbombswholesale? Learn how to assess shelf-life claims, packaging and remaining selling time to protect margins and make smarter purchasing decisions.
 How reshoring affects CNC industry investment in the USAExplore how reshoring shapes CNC industry investment in the USA, from machine purchases and automation to supply chain risks and smarter capital decisions.
 How to keep application engineering support documentation currentKeep application engineering support documentation current with practical guidance on ownership, change control, supplier updates, and reliable handovers.
 When is a scraper chip conveyor system suitable for CNC swarf?Is a scraper chip conveyor system right for your CNC swarf? Explore chip types, coolant filtration, capacity and wear to make a confident choice.
 How to size a CNC surface grinding machine for your workpiecesChoose the right surface cnc grinding machine with practical guidance on travel, clearance, load capacity and accuracy for your workpieces.
 How application engineering support improves product selectionApplication engineering support improves product selection by aligning specifications with real operating conditions. Discover how to compare options with confidence.
 What affects the price of an industrial air compressor?Understand what affects air compressors price, from capacity and controls to installation and energy costs. Compare quotes and choose the best-value system.
 How to check whether a bulletproof vest is NIJ certifiedLearn how to verify bulletproofvests on the official NIJ Compliant Products List, match labels and configurations, and avoid misleading certification claims.
 How to verify organic cotton baby clothes certificationShopping for organiccottonbabyclothes? Learn how to verify GOTS and OCS claims, check certificate details, and choose baby clothing with confidence.
 How to choose a laser level for outdoor workCompare laserlevels for outdoor work by range, accuracy, durability, and receiver compatibility. Find the right tool for reliable results on site.
 How to evaluate an industrial supplier's delivery reliabilityStrengthen industrial procurement support and supplier evaluation with practical checks for delivery records, lead times, capacity, and recovery plans.
 How to inspect welded iron pipes for seam defectsInspect weldedironpipes for seam defects with a practical guide to visual checks, NDT methods, acceptance criteria, and safe repair decisions.
 How to assess electronics manufacturing solutions in North America for production capacityAssess electronics manufacturing solutions North America teams can rely on. Compare capacity, supply risks and quality controls to choose the right production partner.
 Can portable telemedicine devices work with poor connectivity?Telemedicine hardware portable devices can support care with poor connectivity. Discover what works offline and how to evaluate reliable remote care workflows.
 How to choose rugs and carpets for high-traffic roomsDiscover how to choose rugs and carpets for high-traffic rooms. Compare materials, construction, cleaning needs, and fit to find a practical, lasting option.
 What affects the wholesale price of EPS sandwich panels?Compare EPS sandwich panels wholesale prices and discover how core density, steel facings, order size, and delivery costs affect your project budget.
 Why do automatic mechanical watches stop when not worn?Why do automaticmechanicalwatches stop when unworn? Discover how power reserve works, how to restart your watch, and when to seek professional help.
Search News
Popular Tags