When industrial fasteners bolts need traceable material certification
When Industrial Fasteners Bolts Need Traceable Material Certification
When industrial fasteners bolts support safety-critical equipment, material certification is not merely a purchasing attachment. It is the evidence trail that allows quality and safety teams to establish what the bolt is, where its material came from, how it was processed, and whether it was suitable for the duty it was assigned.
That distinction becomes decisive after an incident. A failed bolted joint may be associated with overload, incorrect tightening, hydrogen embrittlement, vibration loosening, corrosion, unsuitable heat treatment, or a substituted material. Without a traceable link between the installed fastener and its production records, the investigation often stops at assumptions. With usable documentation, the team can compare the supplied product against the design specification, applicable code, and actual service conditions.
For routine, low-consequence applications, full batch-level certification may add administrative cost without materially improving risk control. For pressure containment, lifting systems, structural connections, rotating equipment, high-temperature assemblies, or regulated projects, the opposite is usually true: uncertified bolts can create a gap that inspection cannot reliably close later.
A certificate is useful only when it is traceable
The phrase “material certificate” is often used too broadly. A generic statement of conformity, a catalogue declaration, and a mill test report do not provide the same level of control. For industrial fastening, the practical question is whether the document can be connected to the exact lot received and, ideally, to the individual fasteners or packaging units released to the job.
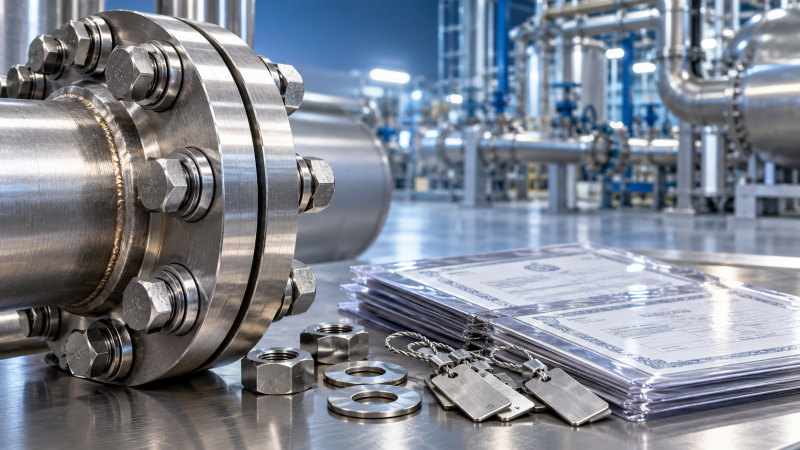
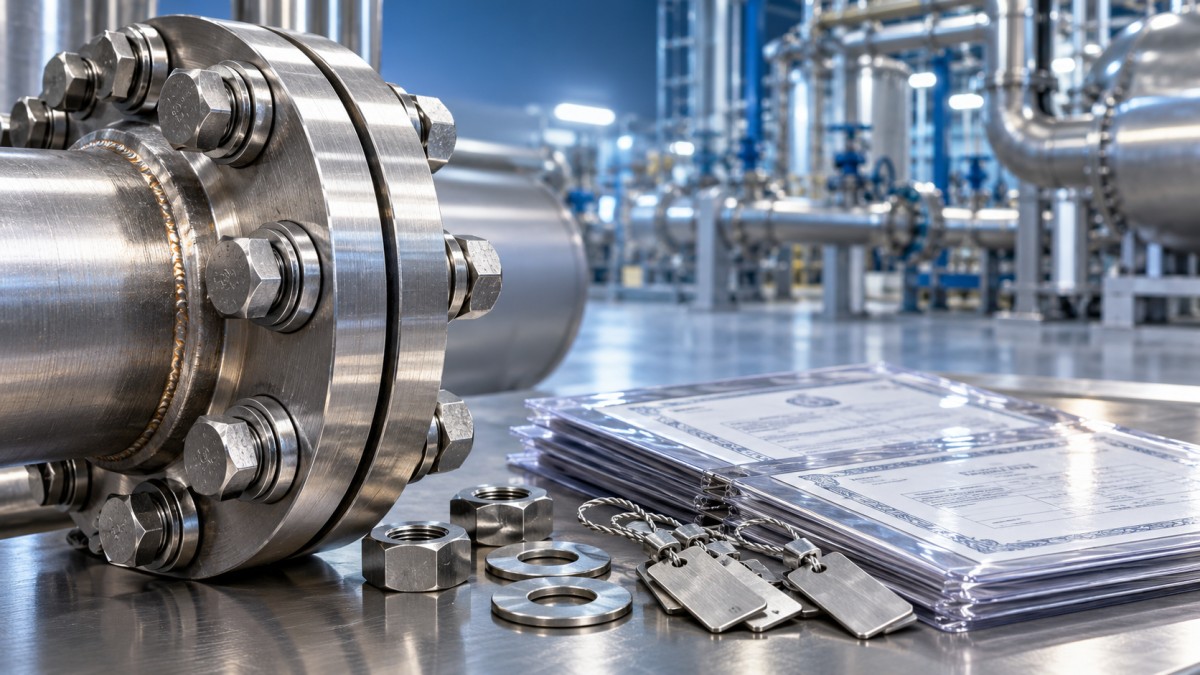
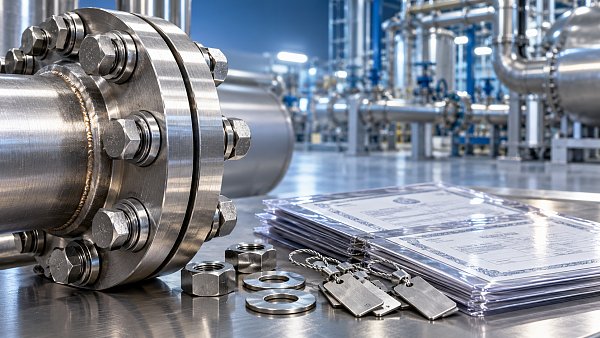
A meaningful traceability chain normally links the purchase order and technical specification to a manufacturer identity, production or heat number, fastener lot number, product designation, dimensions, material grade, applicable standard, test results, and release date. The physical connection may be maintained through markings, tagged containers, sealed packaging, barcodes, or controlled warehouse segregation. If the documents identify a heat number but the delivered bolts cannot be related to that heat number, the paperwork has limited value.
For example, a certificate for stainless steel bar does not automatically certify a finished stud bolt. The finished component may have undergone machining, thread rolling, solution annealing, quenching and tempering, passivation, coating, or other operations that influence its final properties. The required record should reflect the condition in which the fastener is supplied, not simply the condition of its starting stock.
Where traceable certification becomes essential
The need is driven less by the bolt’s unit price than by the consequence of an incorrect bolt. Several situations should trigger a formal certification review before procurement is released.
- Pressure-retaining flanges, valves, piping joints, heat exchangers, and process skids, where bolting performance is part of containment integrity.
- Structural steel, wind-energy equipment, lifting attachments, crane components, and anchor systems where fatigue, preload retention, and specified strength class matter.
- High-temperature or low-temperature service, where the selected alloy and heat treatment must match the design envelope.
- Corrosive atmospheres, offshore installations, chemical processing, marine service, and dissimilar-metal assemblies that require deliberate corrosion-resistance decisions.
- High-vibration machinery such as pumps, compressors, turbines, gearboxes, and heavy rotating equipment, where a loss of preload can escalate quickly.
- Projects governed by a customer specification, an engineering code, an EPC quality plan, or a regulated supply-chain requirement.
In each case, certification does not eliminate the need for sound joint design and controlled installation. A fully certified bolt can still fail if it is overtightened, poorly lubricated, exposed to unexpected media, paired with incompatible nuts, or installed with damaged threads. Certification is one control within a larger bolted-joint management system, but it is the control that establishes the material baseline.
What QA teams should look for in bolt documentation
The certificate should answer specific acceptance questions. Is the stated material grade the one specified? Do chemical composition and mechanical test values correspond to the governing product standard? Is the heat treatment condition declared where it matters? Does the document identify the lot delivered? Are dimensions, thread form, strength class, and coating or surface treatment included in the release information?
For carbon and alloy steel bolts, mechanical properties may include tensile strength, proof load or yield-related values, elongation, reduction of area, and hardness, depending on the applicable standard and product form. For stainless and nickel-based alloys, chemical composition, heat treatment condition, and corrosion-related suitability may deserve closer attention. A grade name alone is not enough: different standards can assign different requirements to products that appear similar in commercial descriptions.
Coatings deserve their own review. Zinc plating, zinc flake systems, phosphate coatings, hot-dip galvanizing, PTFE-based finishes, and other surface treatments affect corrosion performance and tightening behavior. Some processes also require specific controls for high-strength fasteners because of hydrogen embrittlement risk. A certificate that confirms the base material but says nothing about a specified coating cannot confirm that the delivered assembly matches the design intent.
European projects may specify inspection documents under EN 10204. These document types are frequently requested, but they should not be treated as a substitute for a complete technical review. In broad terms, a 3.1 document reports test results validated by the manufacturer’s authorized inspection representative independent of production, while a 3.2 document involves additional validation by the purchaser’s authorized representative or an inspector designated in the applicable requirements. The project specification should state the required document type and the test basis; otherwise, suppliers may provide documents that look formal but do not meet the intended level of verification.
Standards establish the language, not automatic interchangeability
Industrial fasteners bolts are commonly procured against ISO, DIN, ASTM, ASME, JIS, EN, or project-specific requirements. These standards make communication more precise, yet they should not be used as shortcut labels for equivalence. A bolt produced to one standard may differ from another in chemical limits, testing requirements, dimensional tolerances, marking rules, heat treatment, or intended application.
This issue is particularly relevant in international procurement. A purchase order that says only “high tensile bolt” or “stainless bolt” invites interpretation. A stronger specification identifies the relevant fastener standard, nominal size and thread, material or property class, finish, nut and washer requirements, documentation level, traceability method, inspection hold points if needed, and any service restrictions. Where pressure equipment codes or client standards apply, those requirements should take priority over general commercial terminology.
Independent technical review is valuable when several standards meet in one assembly. Global Precision-Machining & Engineering (G-PME) approaches fastening and sealing systems as part of a wider production-risk picture: material integrity, machining quality, fluid-system reliability, and operational uptime are linked. Benchmarking against ISO, DIN, ASME, and JIS references is most useful when it helps a project team identify differences that must be resolved—not when it creates a superficial claim of standard compliance.
The weak points are usually at receiving and installation
Even well-written procurement requirements can fail in the warehouse. Mixed lots, separated certificates, repackaged bolts, missing labels, and partial returns are common sources of traceability loss. Once fasteners from different deliveries enter the same unmarked bin, a later material review may no longer be defensible.
Receiving inspection should therefore verify more than quantity and visible condition. The team should compare packing labels with certificates, verify the stated grade and lot references, inspect required head markings where applicable, preserve documents in the project record, and quarantine discrepancies before material reaches installation. Where individual markings are not feasible because of size or product design, controlled packaging and batch identification become more important.
Installation records matter as well. A bolt certificate cannot demonstrate that the correct tightening method was used. For critical joints, teams may need to retain torque or tensioning records, calibrated tool status, lubrication assumptions, sequence requirements, and inspector sign-off. The technical logic is simple: material properties determine what a fastener can withstand, while assembly control determines the load actually introduced into the joint.
When a certificate should be challenged
A certificate deserves further review if values are incomplete, if the standard cited does not match the order, if the lot number is absent from packaging, or if the material description is vague. Other warning signs include documents covering an implausibly broad product range, handwritten alterations without controlled authorization, inconsistent manufacturer names, or a certificate issued for raw material when the order requires finished fasteners.
When the consequence of error is high, positive material identification, hardness checks, dimensional inspection, or third-party testing may be appropriate. Those measures should be defined by the project quality plan rather than applied indiscriminately. Testing a few samples may identify an obvious substitution, but it does not reconstruct a broken chain of custody for an entire mixed batch.
Specify the evidence before the bolts are made
The most effective time to control certification is before quotation and production, not after delivery. Procurement, QA, engineering, and safety personnel should agree on which joints are safety-critical, which standards govern each item, what document type is required, and how the supplied lot will remain identifiable through receipt and installation.
For low-risk maintenance stock, a manufacturer declaration and sensible supplier qualification may be proportionate. For critical equipment, require traceable material certification, define acceptance criteria, and prevent lot mixing. That approach is not paperwork for its own sake. It gives the organization a practical basis for accepting hardware before it enters service—and a defensible record if its performance must later be questioned.
Recommended News
 How CNC controller cycle time speed affects machining throughputCNC controller cycle time speed can raise machining throughput by sustaining feed rates on complex toolpaths. Learn how to optimize CAM, look-ahead, and machine dynamics.
 When a 4 axis vertical machining center is the better fit than 3-axisDiscover when a 4 axis vertical machining center outperforms 3-axis machining—reduce setups, improve datum control, and boost efficiency for complex multi-face parts.
 When industrial fasteners bolts need traceable material certificationIndustrial fasteners bolts need traceable material certification for critical applications. Learn what QA teams should verify to reduce risk and ensure compliance.
 How to size pump systems for cooling circuits for stable flow ratesPump systems for cooling circuits: learn how to match flow, total dynamic head, NPSH, and controls for reliable, energy-efficient cooling performance.
 When does software as a service reduce CNC data management costs?Software as a service can lower CNC data management costs by reducing IT overhead, manual reporting, and disconnected records. Discover when SaaS delivers measurable savings.
 CNC investment trends 2026: are automation upgrades taking priority?CNC investment trends 2026 reveal why automation upgrades are reshaping capacity plans. Compare robots, pallet systems, and new machines for smarter CNC growth.
 How to size high pressure pumps for stable chemical injection ratesHigh pressure pumps sizing guide for stable chemical injection rates—learn how to balance flow range, pressure, suction conditions, materials, and controls for reliable dosing.
 When organic chemicals are suitable feedstocks for synthetic lubricantsOrganic chemicals can unlock high-performance synthetic lubricants. Learn how purity, stability, compatibility, and supply control shape reliable industrial formulations.
 What machine tool market size reveals about capital spending cyclesMachine tool market size reveals capital spending cycles through order mix, automation, replacement demand, and capacity signals. Discover what drives smarter investment decisions.
 What causes solar inverters to trip repeatedly after installationSolar inverters tripping repeatedly? Discover key causes, from grid voltage and DC faults to wiring, settings, heat, and practical troubleshooting steps.
 How a tool life calculation chart improves cutting parameter decisionsTool life calculation chart insights help optimize cutting speed, feed, and depth for predictable tool changes, better part quality, and lower machining costs.
 What to check before choosing an industrial lubricating oils factoryIndustrial lubricating oils factory selection guide: compare quality control, formulation fit, traceability, technical support, and total cost to reduce downtime risks.
 Where machine shop digital transformation delivers the fastest paybackMachine shop digital transformation delivers faster payback by reducing downtime, setup delays, quality risks, and capacity constraints with focused, measurable workflows.
 When a semiconductor manufacturing solutions provider can shorten process ramp-upA semiconductor manufacturing solutions provider can shorten ramp-up through validated hardware, change control, field support, and resilient supply chains.
 How to evaluate CNC tooling suppliers in Europe for repeatable precisionCNC tooling Europe: learn how to evaluate suppliers for repeatable precision, stable tool life, application support, traceability, and resilient delivery.
 When does manufacturing competitiveness consulting pay off for a plant?Manufacturing competitiveness consulting pays off when plants face costly constraints, capital decisions, quality risks, or supply disruptions. Learn how to build a measurable ROI case.
 How to order acoustic ceiling tiles in bulk without overbuyingAcoustic ceiling tiles bulk buying made simple: calculate accurate quantities, control waste, secure spare stock, and plan phased deliveries to avoid costly overordering.
 Which laboratory microscopes fit routine quality inspection work?Laboratory microscopes for routine quality inspection: compare stereo, digital, compound, and measuring options to improve defect detection, documentation, and throughput.
 Can AI for multi axis machining reduce errors in complex toolpaths?AI for multi axis machining helps reduce complex toolpath errors through smarter collision detection, kinematic analysis, post validation, and machine-data insights. Learn how to improve precision.
 How seamless steel pipes are checked for wall-thickness consistencySeamlesssteelpipes wall-thickness checks explained: learn how ultrasonic scanning, calibration, and tolerance control ensure reliable, pressure-ready pipe quality.
 When a horizontal boring machine for metalworking improves large-part setupHorizontal boring machine for metalworking: learn how stable datums, rotary indexing, and rigid fixturing improve large-part accuracy and setup efficiency.
Search News
Popular Tags